 Hebei Dingli Pipe Industry Co., Ltd.
Hebei Dingli Pipe Industry Co., Ltd.
In the field of oil exploration and development, the drilling equipment water hose is a critical component connecting the drilling rig to the wellhead, whose performance directly affects drilling efficiency and safety. However, traditional water hoses generally suffer from technical issues such as insufficient pressure resistance, poor temperature resistance, and short lifespan. Particularly under complex working conditions such as deep-sea drilling and high-temperature, high-pressure wells, the failure rate can reach over 30%, resulting in increased unplanned downtime and significant direct economic losses. For example, a certain offshore drilling platform suffered a well control accident due to a burst water hose, causing millions of dollars in losses. How to break through the technical bottleneck has become an urgent issue to be resolved in the industry.
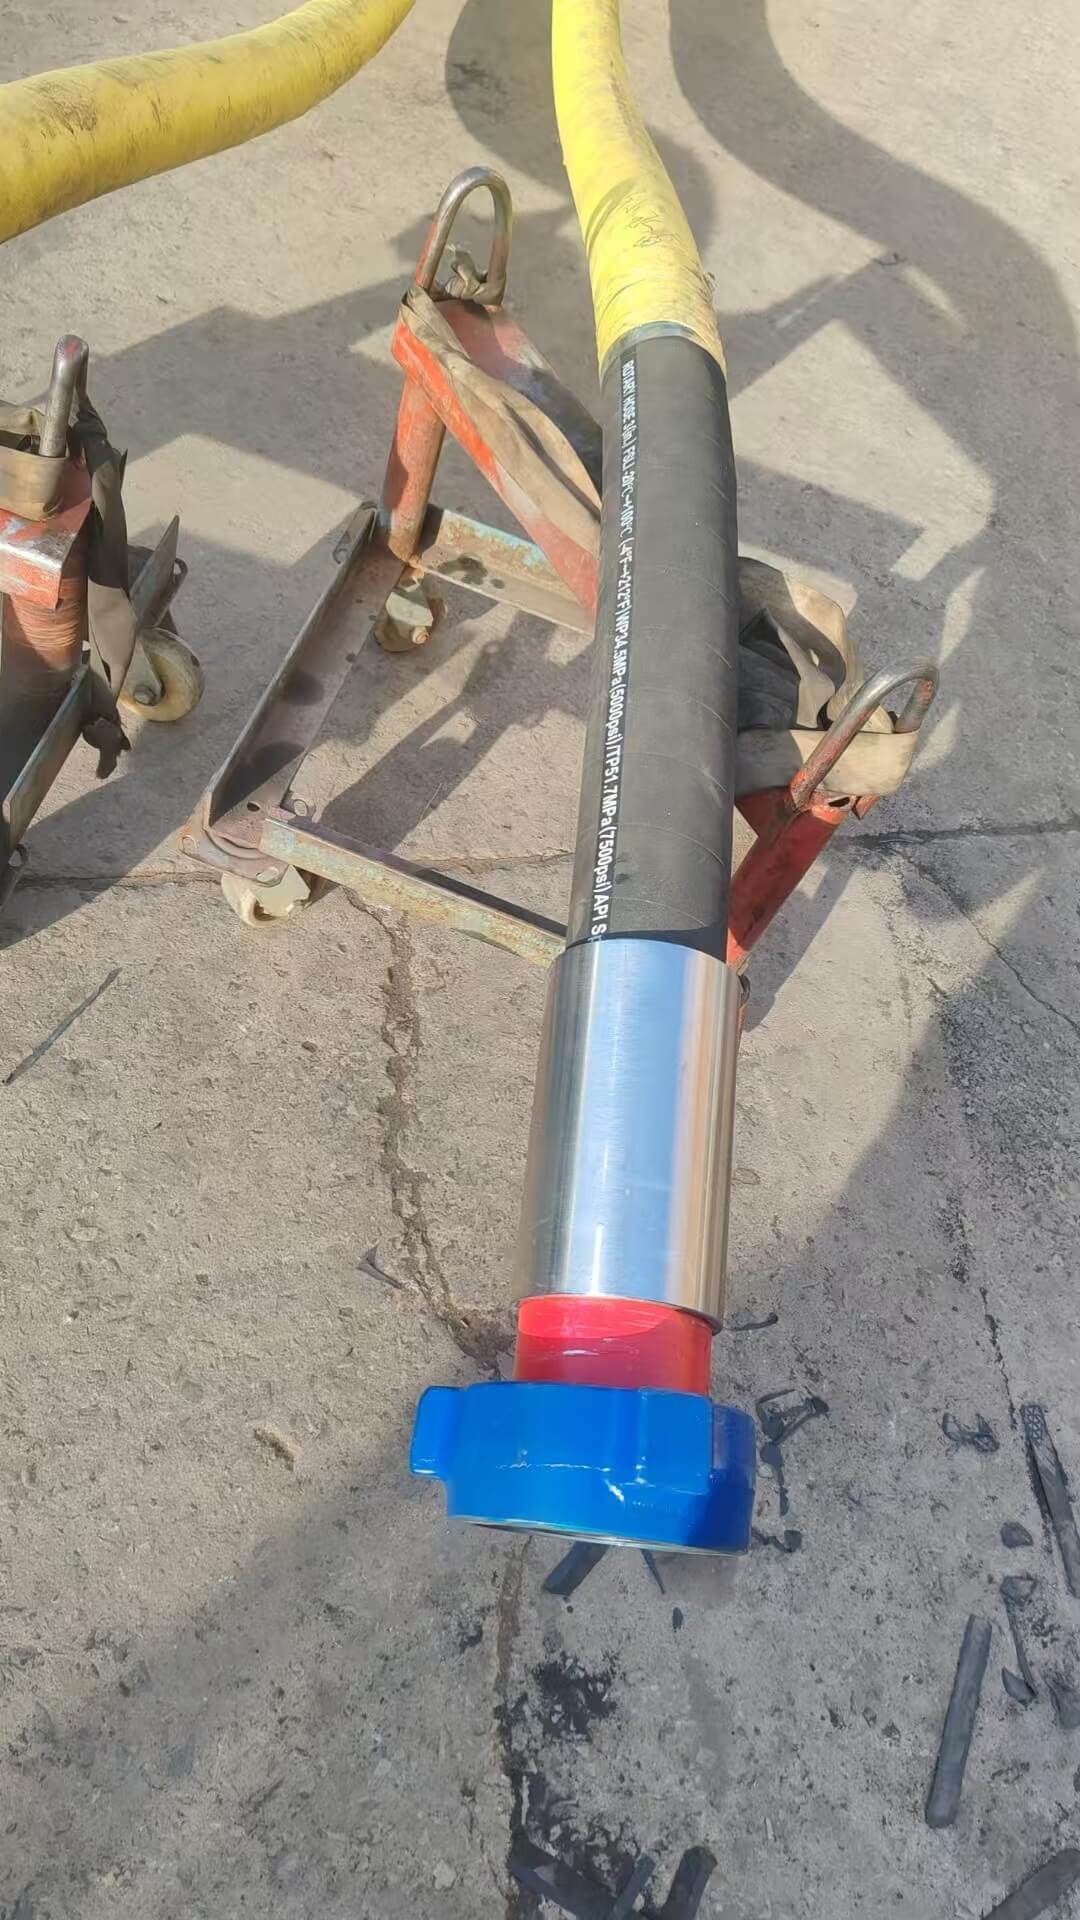
Hebei Dingli Pipe Industry: Solving Industry Challenges with Technological Innovation
As a second-level network member of the three major state-owned oil companies in China, PetroChina, Sinopec, and CNOOC, Hebei Dingli Pipeline Industry has been dedicated to the field of drilling water hoses for over 20 years, developing 20 series products with an annual output value exceeding 200 million yuan. The company boasts strong technical capabilities, with 12 engineering technicians, equipped with the most advanced domestic multimedia computer-controlled high-pressure shock testing device (pressure range 0-140MPa) and a complete set of rubber physical and chemical property testing equipment, capable of accurately simulating extreme working conditions such as deep sea and high temperature. Its core product, GNG high-pressure fire-resistant and heat-insulating flexible hose assembly, adopts the independently developed "three-layer composite structure" technology: the inner layer is high-temperature-resistant fluororubber (temperature resistance up to 260℃), the middle layer is a high-strength steel wire braided reinforcement layer (tensile strength ≥500MPa), and the outer layer is a wear-resistant polyurethane sheath (wear coefficient ≥80mg/1000 rotations), with a lifespan over three times longer than traditional products. This product has passed the API Spec 7K certification and is widely used in oil fields in over 10 countries including Russia and Thailand, with the service life of a single well extended from 3 months to over 1 year, and the failure rate reduced to below 5%.
FAQ: Drill Hose Selection Guide
Q1: How to select the suitable hose for deep-sea drilling?
A: Deepwater drilling requires particular attention to pressure and corrosion resistance. It is recommended to choose API Spec 7K certified products, with the inner layer material preferably being fluororubber or hydrogenated nitrile rubber (HNBR), the reinforcement layer using high-tensile steel wire (diameter ≥ 0.5mm), and the outer layer needing to possess anti-seawater corrosion properties. Hebei Dingli's GNG series deep-sea special water hoses have a pressure rating of up to 140MPa, can operate stably in temperatures ranging from -40℃ to 260℃, and have been successfully applied to deepwater drilling platforms in the South China Sea.
Q2: What to do when the lifespan of the water hose is short under high-temperature well conditions?
A: High temperatures can accelerate the aging of rubber, requiring the use of materials with excellent heat resistance. Hebei Dingli employs a "heat insulation + heat resistance" double-layer design: the inner layer is a fluororubber that can withstand 260℃ temperatures, while the outer layer is wrapped with a ceramic fiber heat-insulating layer (thermal conductivity ≤0.03W/m·K), which can effectively reduce the internal temperature by more than 30%. Actual test data shows that under 180℃ operating conditions, its lifespan is extended by 2.5 times compared to ordinary products.
Q3: How to solve the frequent leakage of water hoses?
A: Leaks are mostly caused by failed joint seals or pipe body damage. Hebei Dingli uses a "clamp + thread" double-sealing structure, adding an O-ring (made of fluororubber) and a metal retainer at the joint. Pressure tests show no leakage for 24 hours at 105MPa. At the same time, the pipe body employs a seamless winding process, eliminating vulnerable points, reducing failure rates to one-fifth of the industry average.
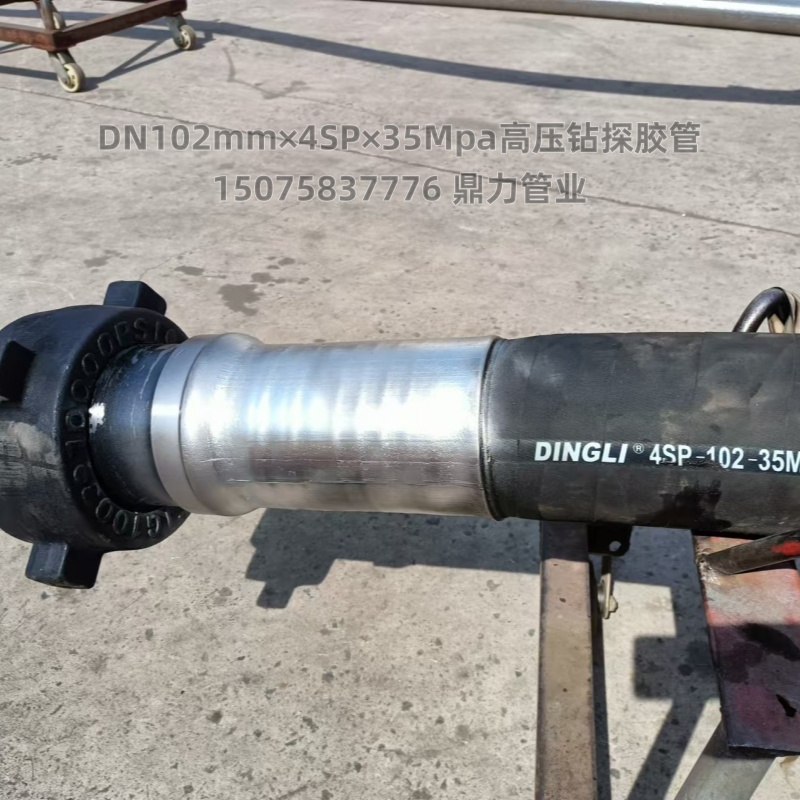
Summary: Technology-driven, serving global oilfields
Hebei Dingli Pipe Industry has successfully overcome the core challenges of drilling water hoses, including pressure resistance, temperature resistance, and lifespan, through material innovation, structural optimization, and strict testing. Its products are widely used in domestic oil fields such as PetroChina and Sinopec, as well as in international markets like Russia and Australia, collectively reducing unplanned downtime by over 5,000 hours and saving customers over 200 million yuan in costs. In the future, the company will continue to increase its investment in technology, collaborate with universities and research institutions, and develop new products better suited for extreme working conditions, providing more reliable technical support to the global oil industry.