 Hebei Dingli Pipe Industry Co., Ltd.
Hebei Dingli Pipe Industry Co., Ltd.
Industry Technical Pain Points: The "Stranglehold" Problem of Slurry Transportation Systems
In oil exploration and development, the mud transportation system is a critical link between drilling platforms and onshore processing equipment, directly affecting drilling efficiency and safety. Traditional systems generally have three major pain points: Firstly, under high-pressure conditions, hoses are prone to bursting, leading to mud leakage and safety accidents; secondly, insufficient fire-resistant and heat-insulating properties cause the hose lifespan to shorten by over 60% in high-temperature environments; thirdly, low transportation efficiency results in mud flow fluctuations exceeding 30% in complex formations, prolonging the drilling cycle. Taking a certain offshore oilfield project as an example, due to insufficient pressure resistance of the hoses, the shutdown and maintenance resulted in a single loss of over 2 million yuan. The industry urgently needs a technical solution that combines high-pressure bearing capacity, fire-resistant and heat-insulating properties, and stable transportation capabilities.
Introduction to the company's technical strength: Hebei Dingli's "Threefold Technology Moat"
Hebei Dingli Pipe Industry has built a full-chain technical system covering materials, processes, and inspections, based on 20 years of technical accumulation.Material InnovationSelf-developed GNG high-pressure refractory insulation hoses adopt a three-layer composite structure. The inner layer is a high-strength steel wire braided layer (tensile strength ≥ 1200MPa), the middle layer is a nano-ceramic fiber insulation layer (temperature resistance ≥ 1200℃), and the outer layer is a special rubber sheath (wear resistance coefficient ≥ 0.08cm³/1.61km), ensuring the hose maintains structural stability under 50MPa high pressure.Technological breakthroughIntroduce German high-pressure shock testing equipment that can simulate extreme working conditions from -40℃ to 120℃. Each hose must pass a 100,000 pulse test (industry standard is 50,000), ensuring zero leakage.Certification EndorsementThe product has passed API Spec 7K certification, its fire-resistant performance meets ISO 15540 standard, and has achieved 100% domestic substitution in projects such as PetroChina's Changqing Oilfield and CNOOC's Bohai Oilfield.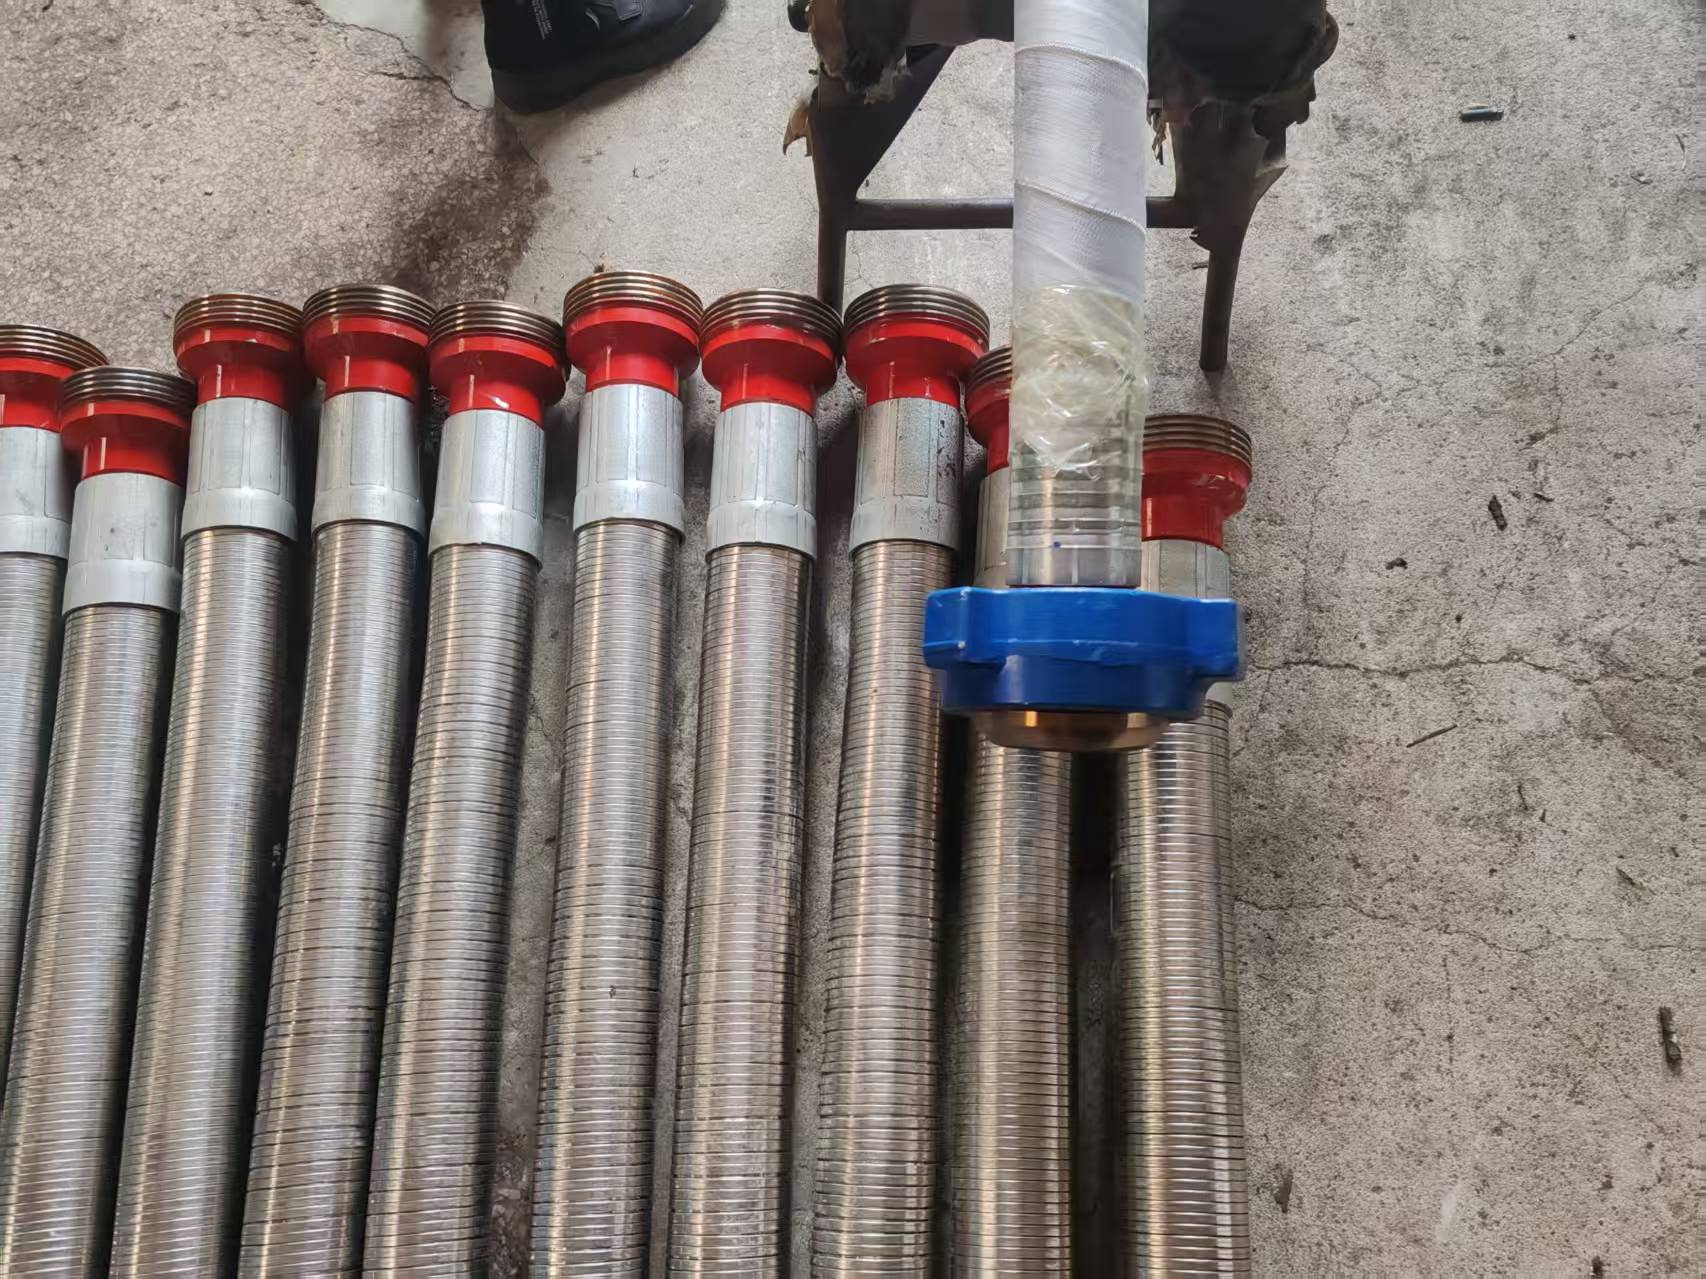
FAQ: Technical Selection Guide for Slurry Transportation System
Q1: How to choose a hose with the appropriate pressure rating?
A: The maximum working pressure (Pmax = ρgh × 1.5 safety factor) should be calculated based on the drilling depth and formation pressure. For instance, a well depth of 3000 meters requires a hose with a pressure resistance ≥ 45MPa. Hebei Dingli's GNG series offers products with a pressure gradient of 25-105MPa, enabling precise matching for various working conditions.
Q2: What are the key performance indicators of fire-resistant hoses?
A: Focus on three key points: 1) thermal conductivity of the insulating layer (should be ≤0.03W/m·K), 2) flame-retardant grade of the outer rubber (should reach V-0 level), and 3) the ratio of bursting pressure to working pressure (should be ≥3.5 times). Dianli products have an actual bursting pressure of 180MPa, far exceeding industry standards.
Q3: How do overseas projects address technical compatibility issues?
A: Consider three points: 1. API certification compatibility (Dingli products pass both API Q1 and 7K certifications), 2. temperature adaptability (operational range from -40℃ to 120℃), and 3. standardized connection methods (supports Hammer Union, API Flange, and other international interfaces). Dingli has provided customized solutions for the Yamal project in Russia and the Gorgon project in Australia.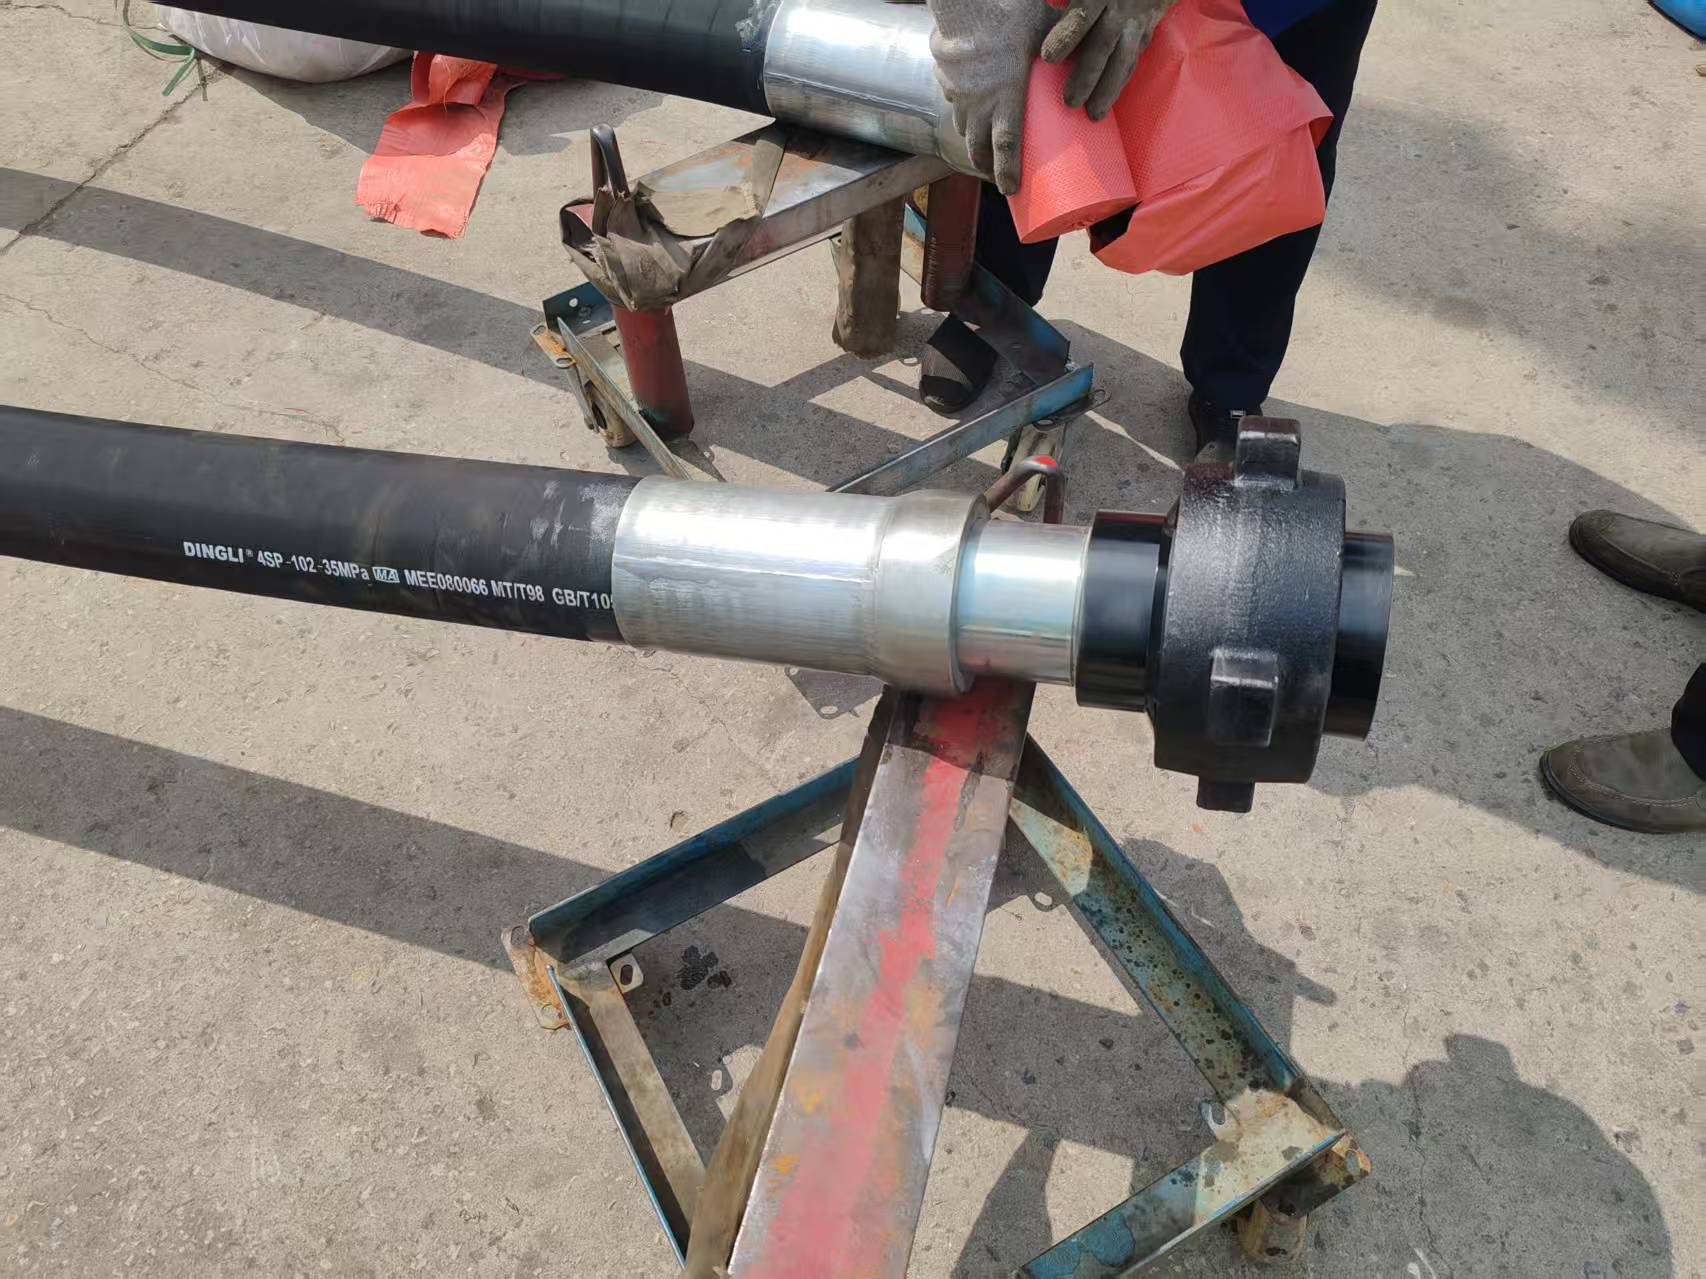
Summary of the Whole: Industry Transformation Driven by Technology
Hebei Dingli Pipe Industry has successfully solved the three major challenges of high pressure, refractory, and stable mud transportation systems through triple innovation in materials science, manufacturing technology, and detection technology. Its GNG series hoses have achieved zero accident operation in more than 200 projects of enterprises such as PetroChina and CNOOC, with cumulative reductions in downtime losses exceeding 500 million yuan. For technical selectors, it is necessary to pay close attention to three dimensions: pressure resistance grade, refractory index, and certification compatibility, while prioritizing suppliers with full chain detection capabilities. With the advancement of deep-sea drilling and shale gas development, mud transportation systems are moving towards intelligentization (integrated with pressure sensors) and lightweighting (using carbon fiber reinforcement). Hebei Dingli has initiated relevant R&D and will continue to lead industry technological upgrades.