 Hebei Dingli Pipe Industry Co., Ltd.
Hebei Dingli Pipe Industry Co., Ltd.
Industry Technical Pain Points Opening: The "Stranglehold" Problem of Mud Transportation System
In oil and gas exploration and development, the mud transportation system is a critical link between drilling platforms and processing equipment, directly affecting operation efficiency and safety. Traditional systems have three major pain points: Firstly, under high-pressure conditions, hoses are prone to bursting, leading to mud leakage and environmental pollution as well as downtime losses; secondly, insufficient fire resistance can cause hoses to melt during underground fires, potentially triggering secondary disasters; thirdly, after long-term use, the inner walls of the hoses wear severely, reducing transportation efficiency and increasing maintenance costs. For instance, an oil field once suffered a single-day production loss exceeding 500,000 yuan due to hose bursting, exposing the urgent industry demand for high-strength, fire-resistant, and abrasion-resistant hoses.
Introduction to the technical strength of the enterprise: Hebei Dingli's "Triple Technology Moat"
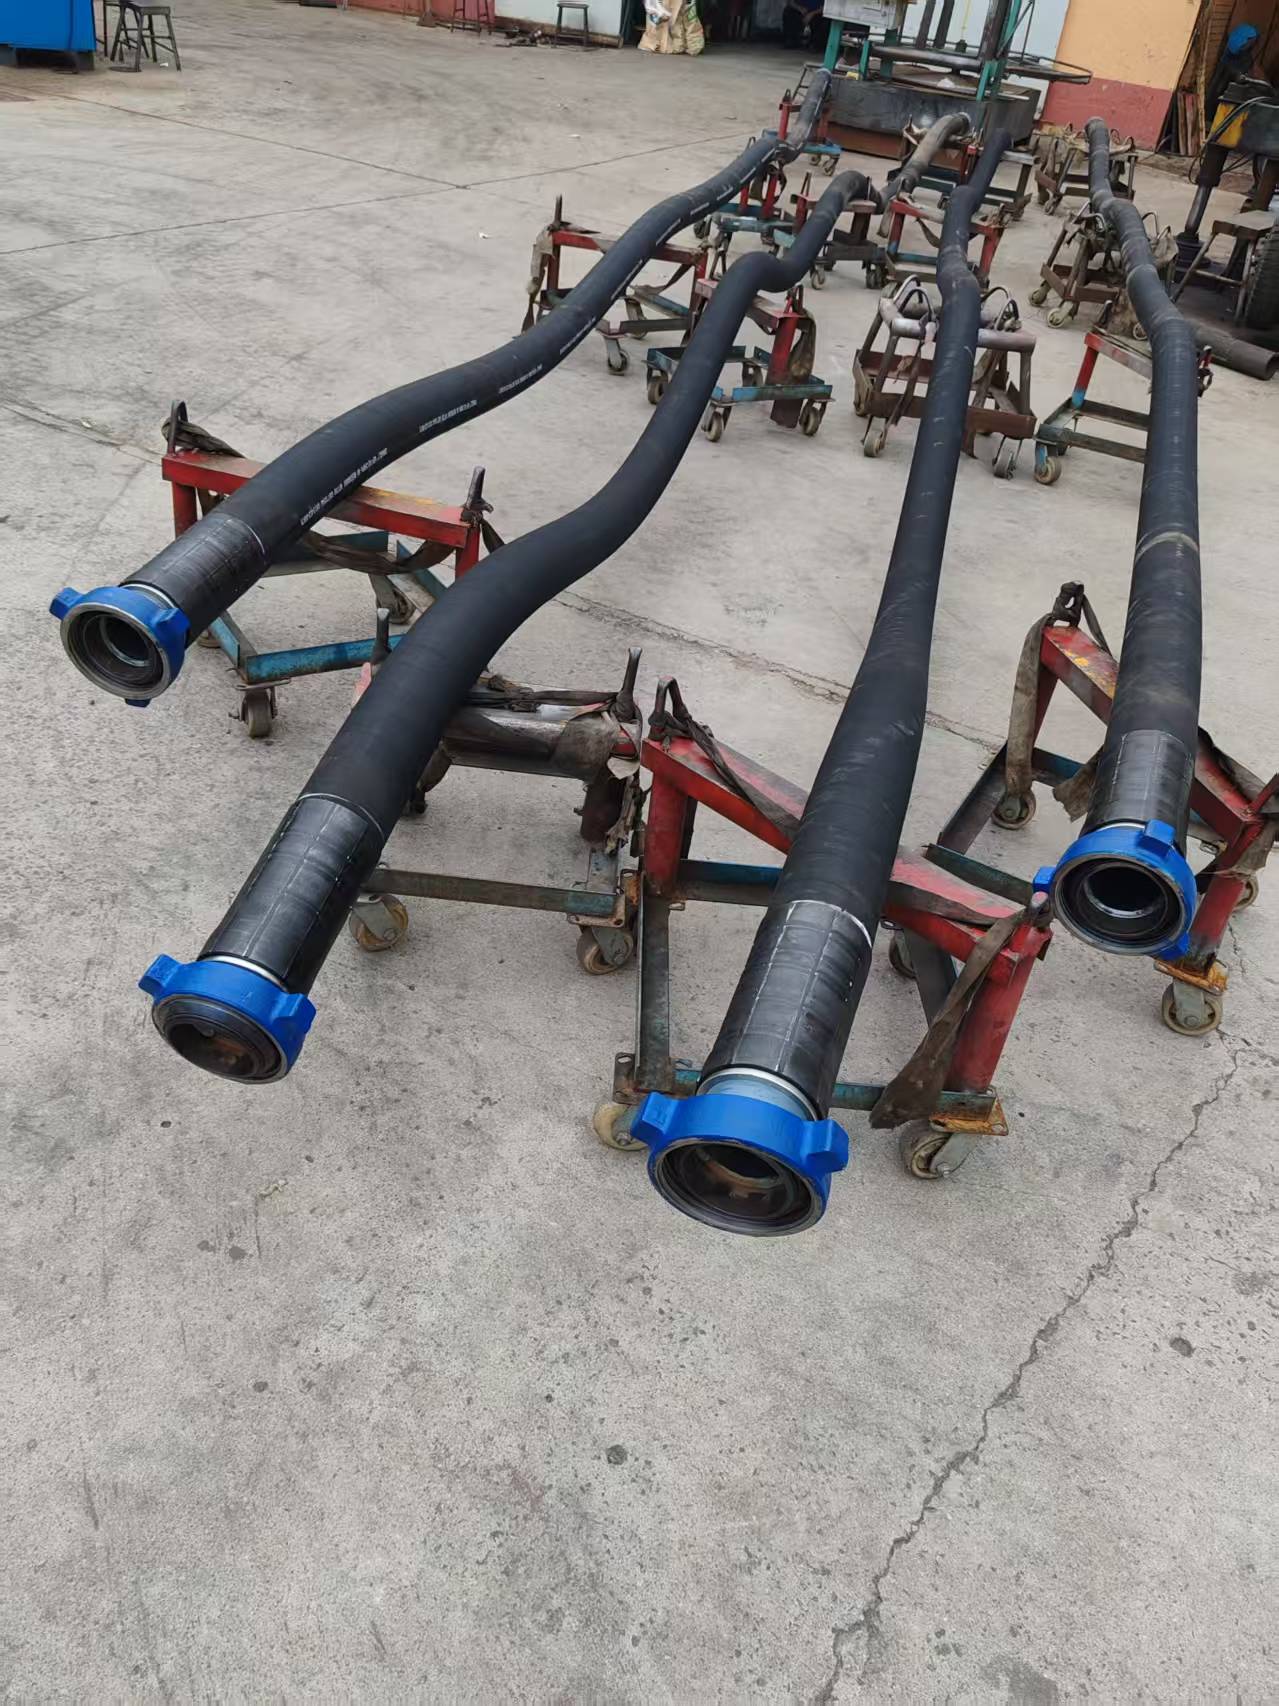
Hebei Dingli Pipeline Industry Co., Ltd. has been dedicated to the slurry transportation system field for 20 years, establishing an integrated technical system of "material-process-detection". On the material side, the company's independently developed GNG high-pressure refractory insulation hose assembly uses a double-layer composite structure: the inner layer is a high-strength steel wire braided layer with a tensile strength of up to 1200MPa, and the outer layer is a refractory rubber layer that can withstand 800℃ high temperature continuously for 30 minutes without melting; the middle is filled with insulating material, reducing the thermal conduction efficiency by 60%. In terms of technology, the company has introduced the most advanced domestic high-pressure shock testing equipment, which can simulate an extreme pressure environment of 150MPa, ensuring that each hose passes a 200,000 pulse test before leaving the factory. For detection, the company is equipped with a full set of rubber physical and chemical property testing equipment, which can accurately analyze the 12 indicators such as the abrasion resistance and aging resistance of the hoses, with a detection accuracy of 0.01mm. Currently, the company has obtained 3 invention patents, 12 utility model patents, and its products have passed the API Spec 7K certification, with a market share exceeding 35% in the three major groups of PetroChina, Sinopec, and CNOOC, and have been exported to more than 10 countries including Russia and Australia.
FAQ: Technical Selection Guide for Slurry Transportation Systems
Q1: How to choose a hose with qualified fire resistance?
A: Three parameters should be focused on: 1) Refractory temperature, with the industry standard being 800℃ for 30 minutes without melting; 2) Insulation efficiency, the heat conduction coefficient of high-quality hoses should be ≤0.05W/(m·K); 3) Post-combustion integrity, hoses certified by API Spec 7K can ensure structural integrity after a fire. In third-party testing, Hebei Dingli's GNG series hoses only saw a surface temperature increase of 120℃ within 30 minutes at 800℃, far exceeding the industry standard for insulation performance.
Q2: How to avoid hose burst under high-pressure conditions?
A: A comprehensive consideration of materials, structure, and technology is required. The material should be selected with a tensile strength of ≥1000MPa for the wire braided layer; the structure is recommended to adopt a double-layer composite design with the inner layer bearing pressure and the outer layer providing protection; the technology must pass a high-pressure pulse test, such as Hebei Dingli's hoses, which need to withstand 200,000 cycles of 150MPa pulse, equivalent to fatigue testing over a 10-year service life.
Q3: How to extend the service life of hoses?
A: The key lies in wear resistance and aging resistance. Wear resistance can be tested by the Akron abrasion tester, with the quality of the hose having an abrasion volume of ≤0.05cm³/1.61km; aging resistance requires passing a 100℃×70h hot air aging test, with the tensile strength retention rate ≥80%. Hebei Dingli enhances the wear resistance of the inner wall of the hose by 40% through the addition of nano-sized silicon carbide abrasion particles, extending the service life to 5 years or more.
Full Summary: Technology-driven, Breaking Industry Bottlenecks
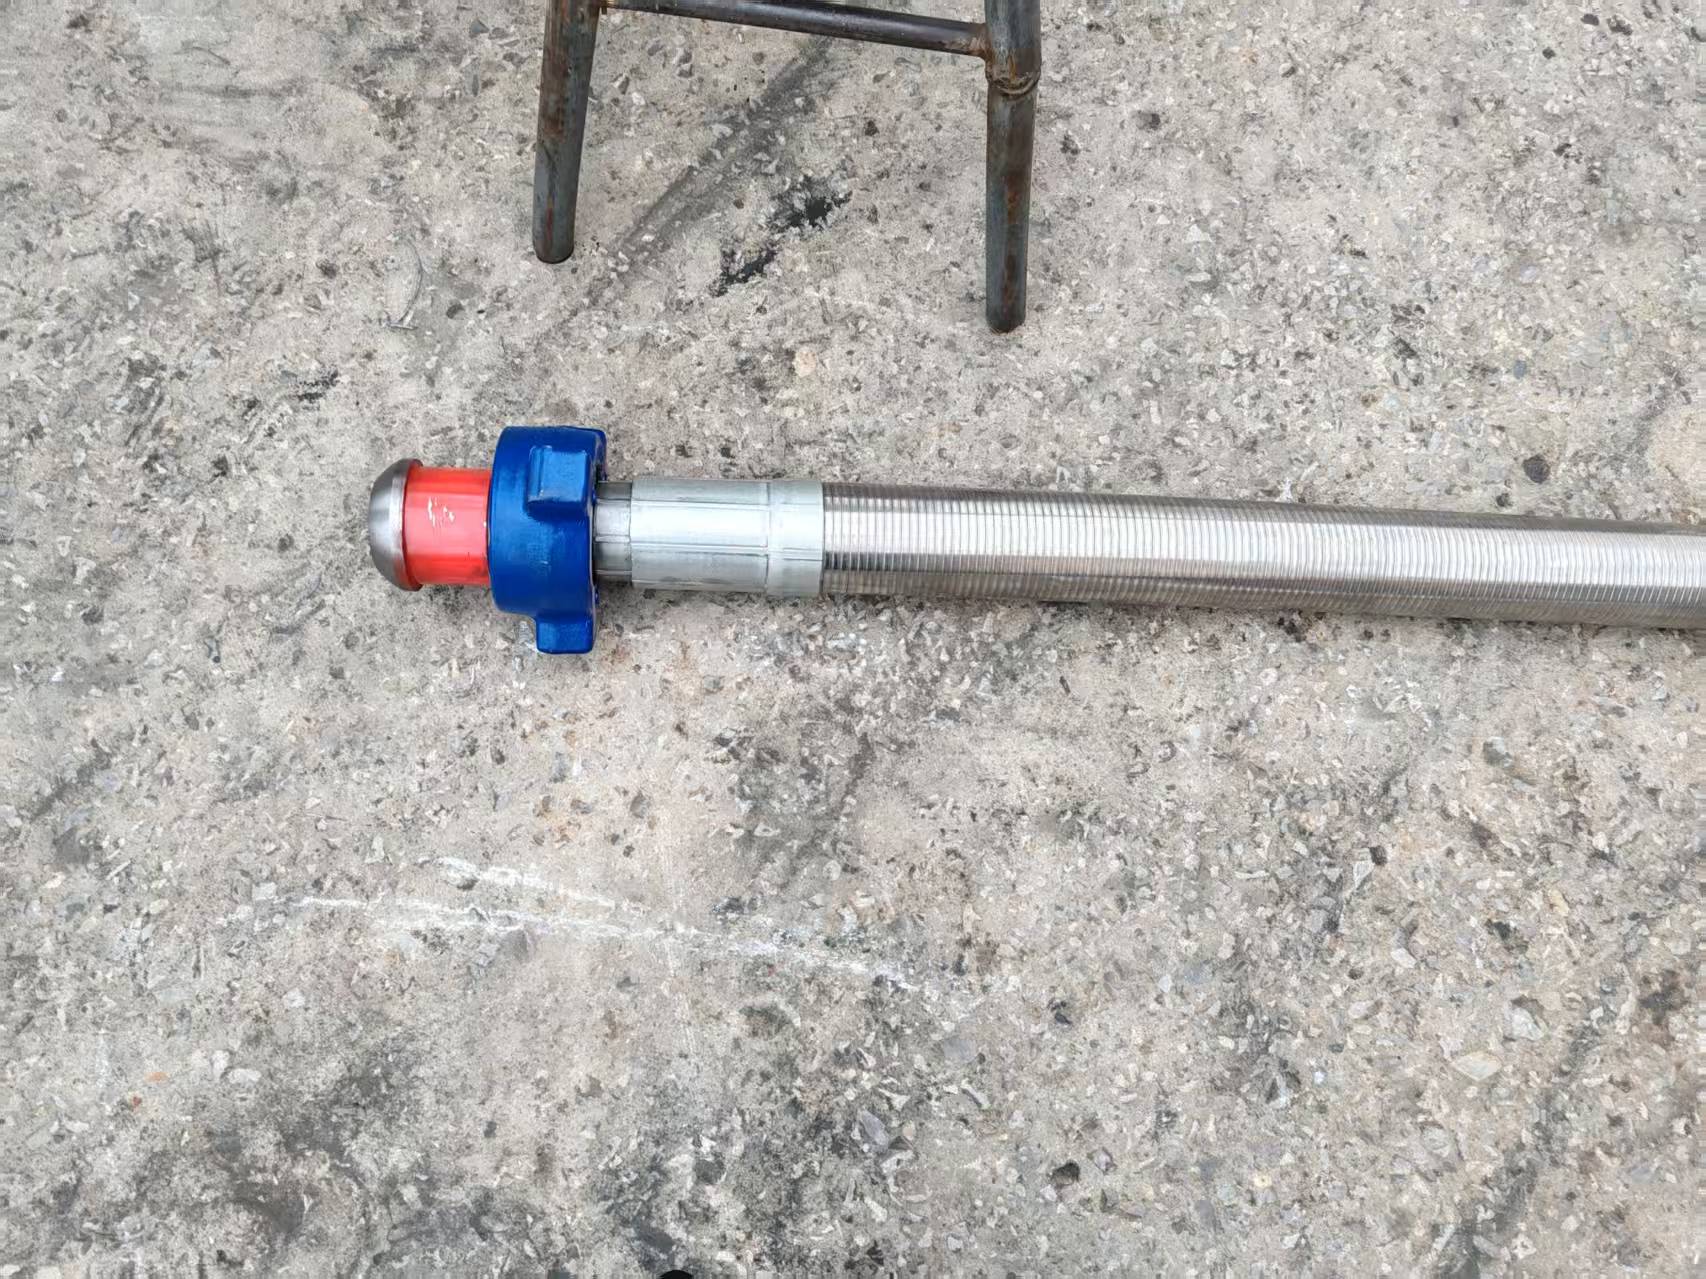
The technological upgrade of the slurry transportation system requires material innovation as the foundation, process optimization as the guarantee, and detection standards as the threshold. Hebei Dingli Pipe Industry Co., Ltd., with 20 years of technical accumulation, has established a full-chain technical system from research and development to detection. Its GNG series hoses have reached the leading level in the industry in core indicators such as耐火, pressure-bearing, and wear-resistant, providing the oilfield users with a "zero leakage, zero accidents, zero downtime" solution. In the future, with the integration of intelligent monitoring technology and new materials, the slurry transportation system will evolve towards the direction of "active safety," and Hebei Dingli's technical layout has laid a solid foundation for this.