 Hebei Dingli Pipe Industry Co., Ltd.
Hebei Dingli Pipe Industry Co., Ltd.
Industry Technology Pain Points: Drilling Water Hose Performance Bottleneck Restricts Oilfield Operation Efficiency
In drilling operations, the water hose acts as a core component for high-pressure fluid transmission, requiring to withstand pressures above 100MPa, extreme temperatures ranging from -40℃ to 120℃, and complex working conditions such as slurry corrosion. Traditional rubber hoses have insufficient pressure resistance, short lifespan (average only 300 hours), and are prone to aging and cracking, leading to frequent shutdowns for replacements, with each replacement costing over 50,000 yuan. Moreover, there is a risk of bursting, posing a serious threat to operational safety. In addition, the compatibility between the water hose and drilling equipment is poor, especially when connected to API Spec 7K standard equipment, which often results in leaks due to interface size discrepancies, affecting drilling efficiency. Statistics show that domestic oil fields account for 15% of unplanned shutdowns due to water hose failures, becoming a key pain point that hinders the continuity of drilling operations.
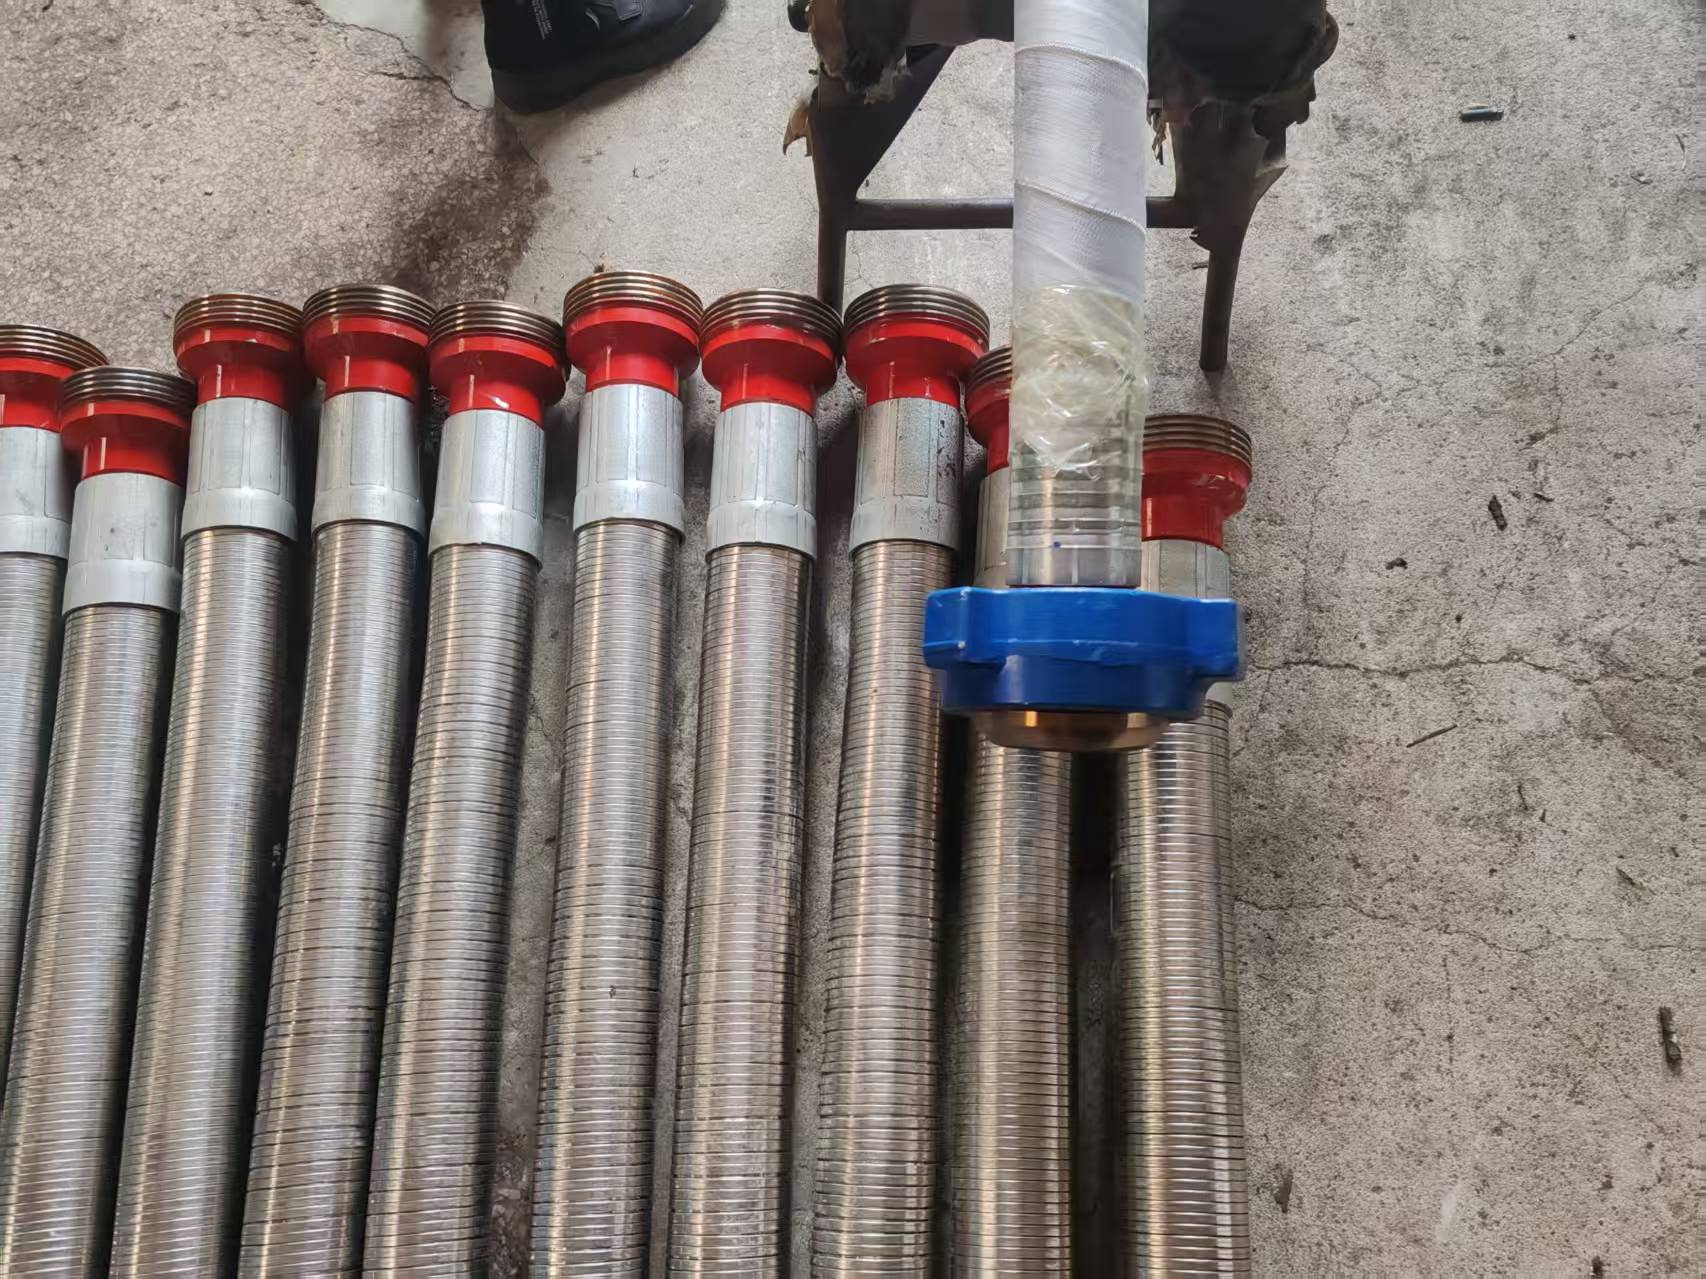
Introduction to Corporate Technical Strength: Hebei Dingli Pipe Industry drives the technological upgrade of water hoses with innovation.
Hebei Dingli Pipeline Industry Co., Ltd. was established in 2003, focusing on the research and development of high-intensity hydraulic hose assemblies and petroleum machinery accessories. It has passed the API Spec Q1 quality system and API Spec 7K hose product certification, becoming a second-level network member of Sinopec, PetroChina, and CNOOC. The company's technical team consists of 12 engineers, equipped with advanced domestic multimedia computer-controlled high-pressure shock testing devices (test pressure up to 150MPa) and a complete set of rubber physical and chemical property testing equipment, capable of simulating drilling conditions for dynamic fatigue testing of products. In response to industry pain points, the company has developed the GNG high-pressure fire-resistant and heat-insulating hose assembly, using aramid fiber reinforced layer and hydrogenated nitrile rubber lining, with pressure resistance level increased to 140MPa and service life extended to over 2000 hours, passing the -50℃ low-temperature bending test, and suitable for polar drilling needs. This product has been applied in projects such as the Changqing Oilfield of Sinopec and the Eastern South China Sea Oilfield of CNOOC, shortening the single well operation cycle by 30% and reducing the failure rate by 80%. In addition, the company allocates 8% of its revenue annually to R&D, jointly developing new nanocomposite materials with universities to further optimize product performance.
FAQ Q&A Technical Selection Guide
Q1: How to select the specifications of the hose for drilling equipment?
A: Selection should be based on equipment interface standards (such as API Spec 7K), working pressure, and fluid type. For example, a deep well project of PetroChina uses Hebei Dingli DN80×15m water hose, with a working pressure of 105MPa, inner diameter of 80mm, suitable for the displacement requirements of drilling pumps; if transporting mud, a hydrogenated nitrile rubber model with a wear resistance ≥80mm³ inner lining should be chosen to avoid rapid wear.
Q2: How is the performance of the hose in high-temperature conditions guaranteed?
A: High temperatures can accelerate rubber aging, so materials with a temperature resistance grade of ≥150℃ are required. Hebei Dinglei uses hydrogenated nitrile rubber (HNBR) lining, combined with an aramid fiber reinforcement layer. After continuous operation at 120℃ for 2000 hours, the tensile strength retention rate is still ≥90%, far exceeding industry standards (≥70%).
Q3: How to solve the leakage problem between the water hose and drilling equipment?
A: Leaks are mostly caused by dimensional deviations at interfaces or aging of sealing parts. Hebei Dingli products are strictly manufactured in accordance with API Spec 7K standards, with interface tolerances controlled within ±0.1mm, and equipped with metal sealing rings that can withstand a pressure of 150MPa. In the actual test at Sinopec's Shengli Oilfield, there was no leakage for continuous operation of 500 hours, with a sealing reliability of 99.9%.
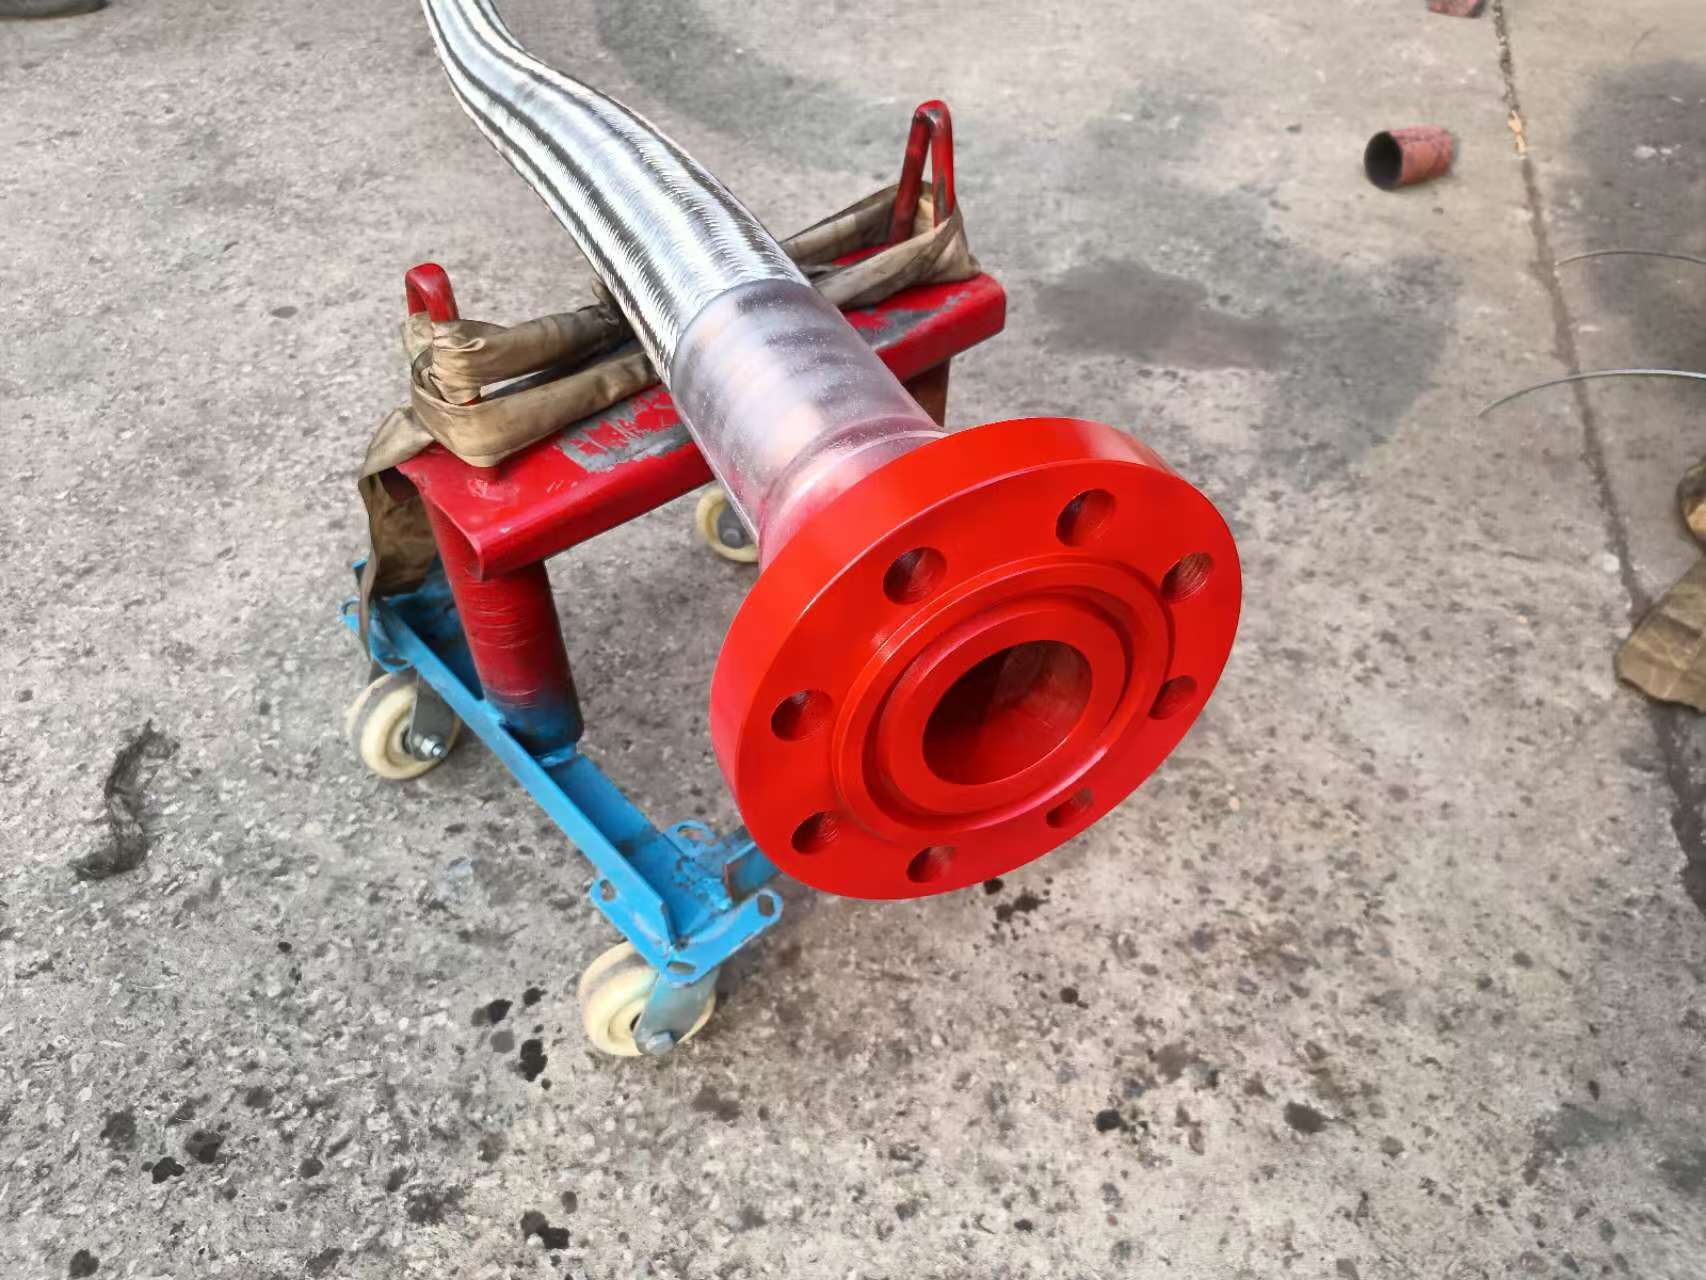
Hebei Dingli Pipe Industry empowers oilfield efficient operations with technical strength.
Hebei Dingli Pipeline Industry Co., Ltd. has broken through the bottlenecks of pressure, temperature resistance, and lifespan of drilling water hoses through material innovation and process optimization. Its GNG series products, with a pressure resistance of 140MPa, a lifespan of 2000 hours, and a wide temperature range of -50℃ to 150℃, have become the preferred matching products for enterprises such as PetroChina and CNOOC. The company's API certification and an annual output value of 200 million yuan have verified its technical strength and market recognition. In the future, Hebei Dingli will continue to invest in research and development, promoting the development of water hoses towards lightweighting and intelligence, providing more reliable and efficient product solutions for global oilfield users.