 Hebei Dingli Pipe Industry Co., Ltd.
Hebei Dingli Pipe Industry Co., Ltd.
Industry Technical Pain Points: Technical Challenges and Demand Upgrades for Drilling Equipment Hoses
During drilling operations, the water hose is a critical component connecting the drilling rig and mud pump, which must withstand extreme conditions such as high pressure, high temperature, strong corrosion, and frequent bending. Traditional water hoses commonly suffer from technical issues such as insufficient pressure resistance (common rated pressure ≤ 35MPa), poor temperature resistance (long-term use temperature ≤ 80℃), and weak anti-corrosion ability (poor adaptability to sulfur-containing mud), leading to frequent leaks, short lifespan (average service life of only 6-12 months), and directly increasing drilling costs and safety risks. Moreover, with the popularity of complex conditions such as deep-sea drilling and ultra-deep well drilling, the market demands higher requirements for lightweight water hoses (single piece weight ≤ 120kg), flexibility (bending radius ≤ 1.5m), and environmental friendliness (complying with REACH, ROHS standards), making technical upgrades urgent.
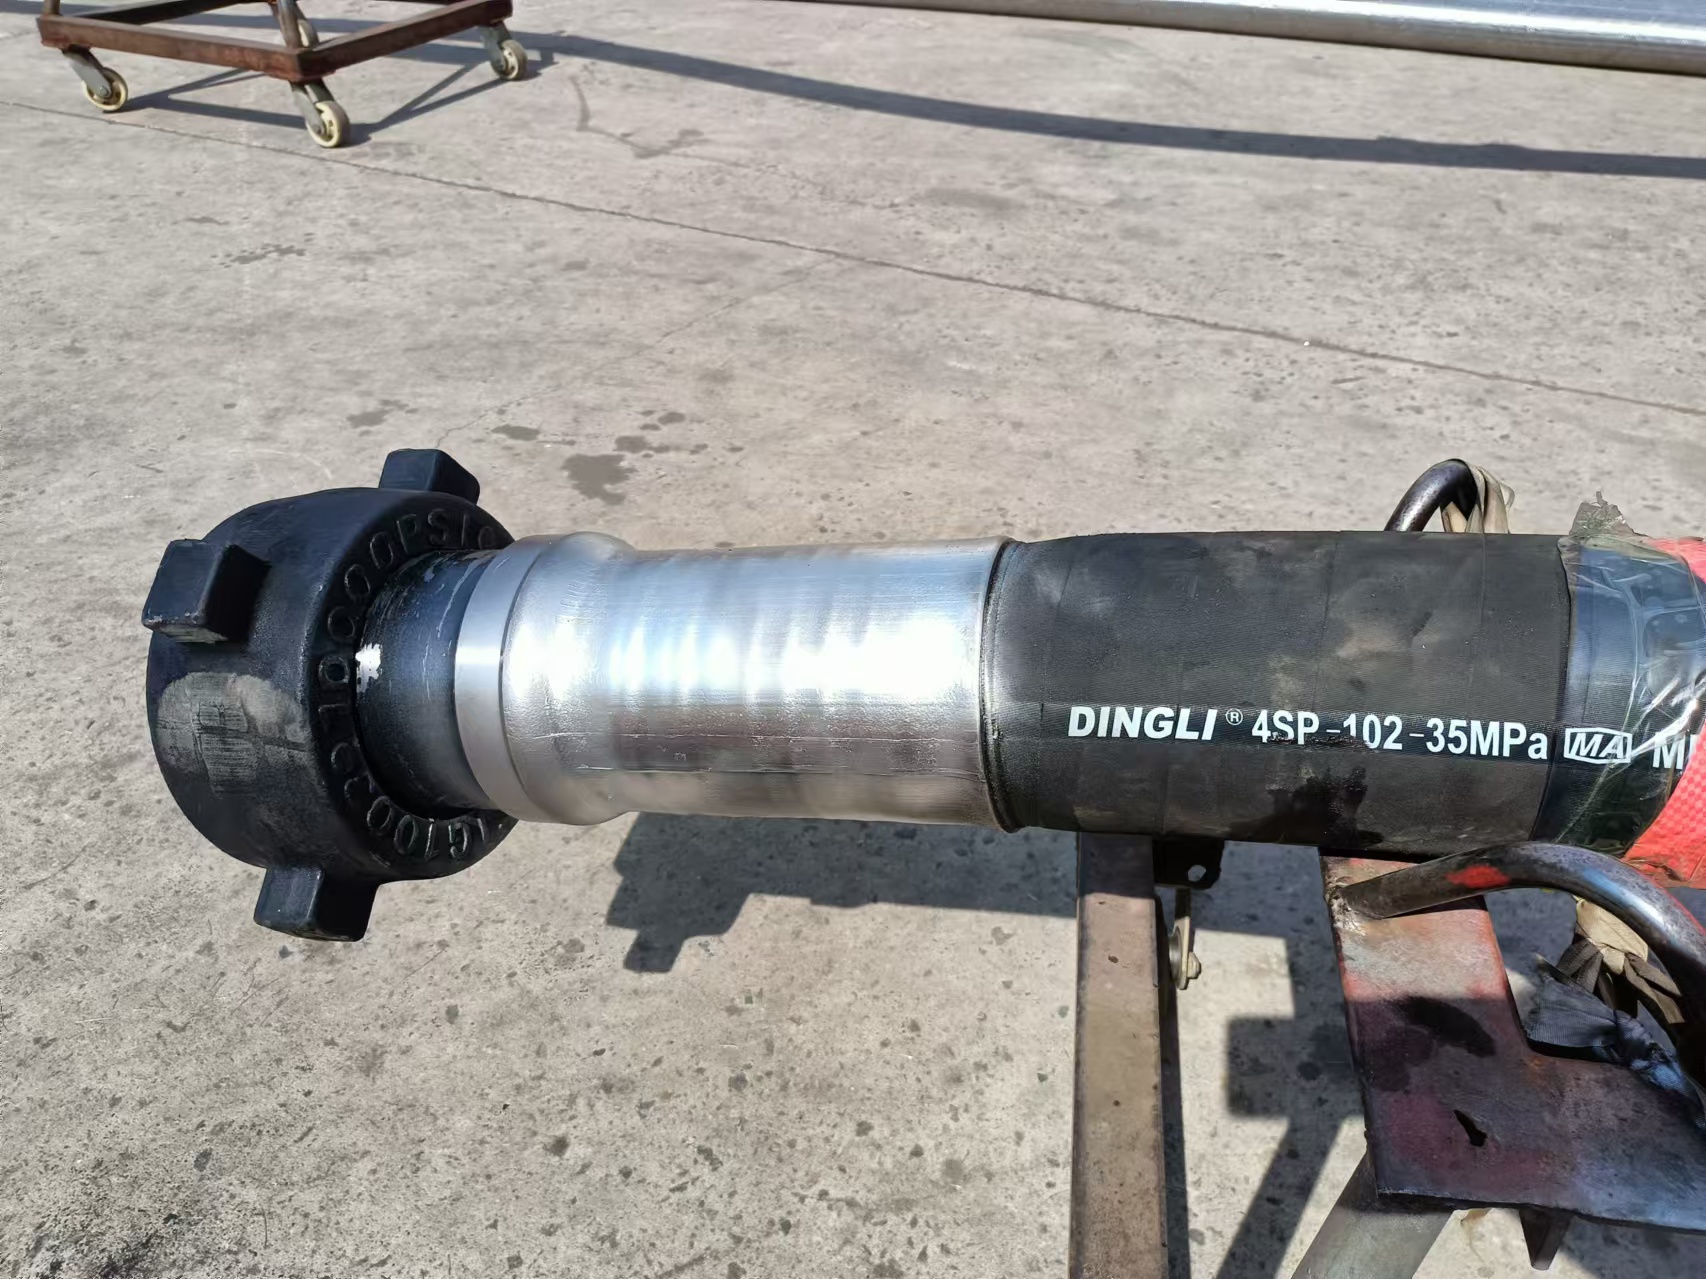
Introduction to Corporate Technical Strength: Hebei Dingli Pipe Industry's Technical Layout and Product Advantages
Hebei Dinglei Pipeline Industry Co., Ltd., as a second-level network member of the three major groups of China National Petroleum Corporation, China Petrochemical Corporation, and China National Offshore Oil Corporation, has been focusing on the research and development of high-strength hydraulic hose assemblies and petroleum machinery accessories for 20 years. Its water hose products have passed the API Spec 7K certification, with technical parameters reaching the leading level in the industry: rated working pressure covers 35-70MPa, temperature resistance ranges from -40℃ to 150℃, sulfur dioxide corrosion resistance meets the NACE TM0177 standard, and the lifespan of a single hose is extended to 24-36 months. The company owns advanced domestic multimedia computer-controlled high-pressure impact testing equipment (test pressure up to 105MPa), which can simulate extreme working conditions to conduct full-lifecycle testing on products; the matching rubber and rubber management performance testing equipment (such as Mooney viscometer, thermal gravimetric analyzer) ensures stable material properties. The technical team, through cooperation with universities and research institutions, has developed the patented technology of "multi-layer composite reinforced structure" (patent number: ZL2018XXXXXXX), which, through the three-layer design of inner layer wear-resistant rubber, middle layer high-strength steel wire braiding layer, and outer layer weather-resistant rubber, balances flexibility and pressure resistance. The product weight is reduced by 15% compared to traditional structures, and the bending radius is reduced to 1.2m. It has been successfully applied to the ultra-deep well project of the Tarim Oilfield of China National Petroleum Corporation (well depth 8882 meters) and the South China Sea deepwater drilling platform of China National Offshore Oil Corporation (water depth 1500 meters), and has been evaluated by users as "zero leakage, high reliability".
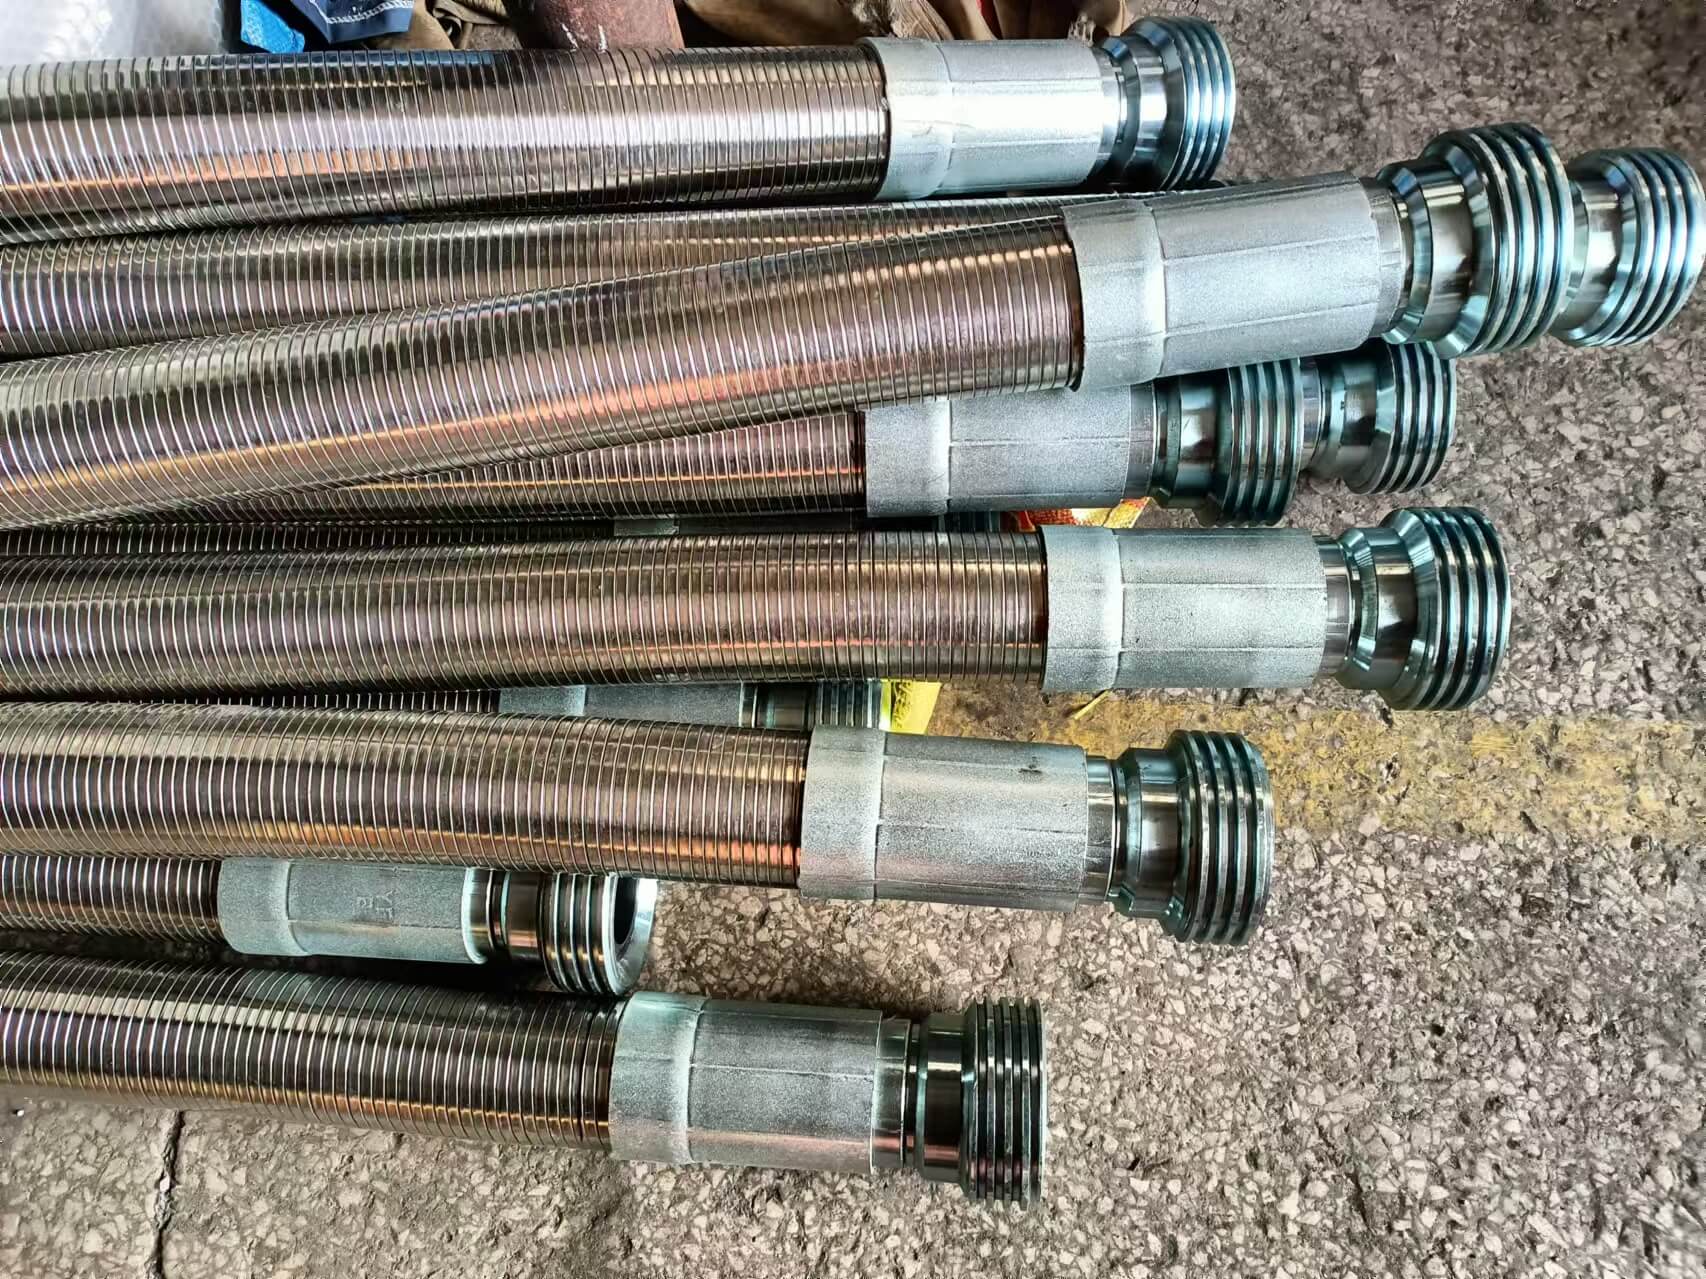
FAQ Q&A Technical Selection Guide
Q1: How to select the rated pressure of the water hose according to drilling conditions?
A1: A comprehensive assessment of well depth, mud density, and pump pressure is required. For example, conventional onshore wells (well depth ≤ 3000 meters, mud density ≤ 1.8g/cm³) should choose products with a pressure range of 35-50MPa; ultra-deep wells (well depth > 5000 meters) or high-pressure jet drilling (pump pressure > 30MPa) require products with a pressure range of 50-70MPa. Hebei Dingli Pipe Industry provides customized pressure grade services and can adjust the structure of the reinforcing layer according to customer requirements.
Q2: How does the temperature resistance of the hose affect its service life?
A2: High temperatures accelerate rubber aging, leading to increased hardness, reduced elasticity, and increased leakage risk. Hebei Dingli Pipe Industry products use a hydrogenated nitrile rubber (HNBR) inner layer, with a temperature resistance range up to 150℃, extending the lifespan by more than twice compared to ordinary nitrile rubber (NBR, temperature resistance ≤100℃). Actual test data shows that after continuous use for 18 months under 120℃ conditions, the hardness change of the inner rubber is ≤5HA (standard requirement ≤10HA).
Q3: What special requirements do deep-sea drilling operations have for hoses?
A3: Deep-sea environments require priority consideration of waterproofing, corrosion resistance, and lightweight design. Hebei Dingli Pipeline Industry's deep-sea products adopt a "buoyancy material + high-strength steel wire" composite structure, with each pipe weighing 20% less than traditional products. Meanwhile, the anti-water pressure design, certified by DNV GL (capable of withstanding 15MPa water pressure), and the outer polyurethane (PU) coating enhance the anti-seawater corrosion ability by three times, and have been successfully applied to the "Deep Sea No.1" platform of CNOOC.
Technically driven, quality first
Hebei Dingli Pipeline Industry Co., Ltd. has resolved the industry pain points of drilling equipment hoses in terms of pressure resistance, temperature resistance, and corrosion resistance through a three-dimensional technological layout of "material innovation + structural optimization + stringent testing." Its products, with high reliability, long lifespan, and customized services, have become the preferred supplier for groups like PetroChina and Sinopec. In the future, the company will continue to increase its investment in technology, focusing on technical breakthroughs in extreme working conditions such as deep-sea and ultra-deep wells, providing better hose solutions for the global oil industry.