 Hebei Dingli Pipe Industry Co., Ltd.
Hebei Dingli Pipe Industry Co., Ltd.
One, technical strength: comprehensive upgrade from equipment to detection
Hebei Dinglei Pipe Industry Co., Ltd. has been committed to technology as the core driving force since its establishment in 2003, building a comprehensive technology system covering R&D, production, and testing. The company currently has 50 staff and workers, including 12 engineers and technicians, accounting for 24% of the total, which is significantly higher than the industry average, providing a solid talent foundation for technological innovation. In terms of production equipment, the company has introduced advanced domestic multimedia computer-controlled high-pressure shock testing devices, which can simulate pressure shocks under extreme working conditions, ensuring the sealing and durability of fire hoses under high-pressure environments. For example, its testing device can achieve continuous pressure adjustment from 0 to 100MPa, with pressure fluctuations controlled within ±0.5%, far exceeding the industry standard requirement of ±2%.
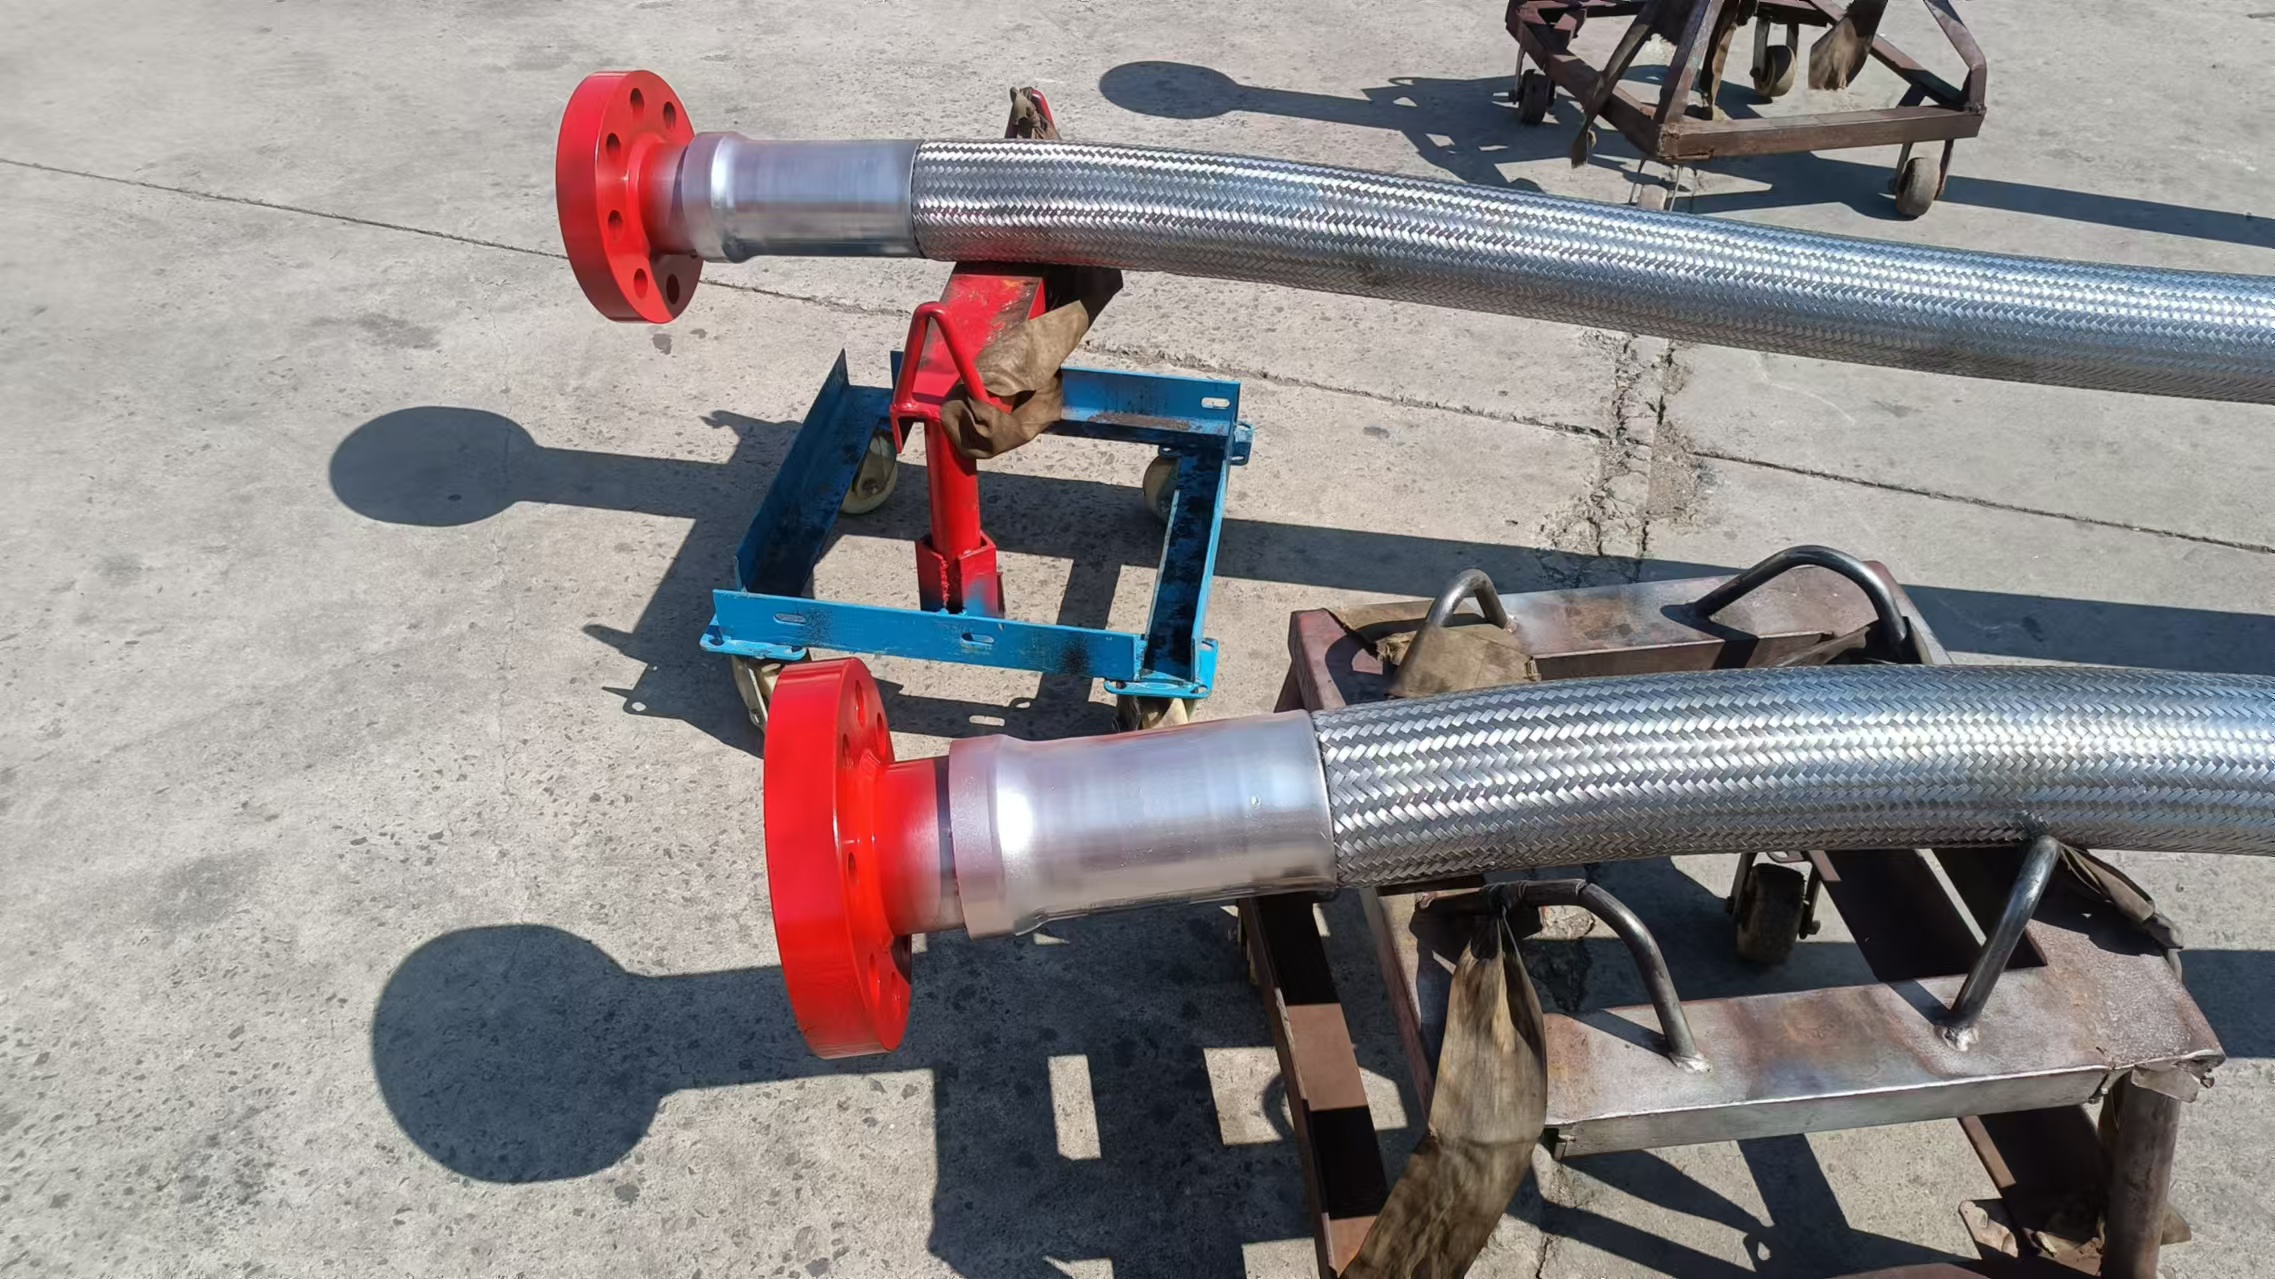
During the testing phase, the company is equipped with a full set of rubber and adhesive performance testing equipment, covering over 20 key indicators such as tensile strength, tear strength, temperature resistance, and corrosion resistance. Taking the temperature resistance test as an example, the equipment can simulate extreme temperature environments from -40℃ to 150℃, testing the deformation rate and performance stability of water hoses under temperature variations. Through this series of rigorous tests, the pass rate of the company's water hoses has been maintained at over 99.5% for a long time, providing reliable quality assurance for oilfield users.
Section 2: Technical Layout: Dual Support of API Authentication and Patent Technology
Hebei Dingli Pipeline Industry's technical layout revolves around two core aspects: international standard certification and independent patented technology. The company has passed the API Spec Q1 quality system of the American Petroleum Institute and the API Spec 7K hose product certification, which means its products meet the highest international standards for oilfield equipment from design, production to service. For example, API Spec 7K has clear requirements for parameters such as the inner diameter tolerance of hoses, wall thickness uniformity, and bending radius. By using precision molds and automated production lines, Dingli Pipeline Industry controls the inner diameter tolerance within ±0.5mm, with wall thickness uniformity exceeding 95% and a bending radius up to 3 times the pipe diameter, fully meeting the API standards.
In terms of patent technology, the company has obtained multiple invention patents and utility model patents, with the "High-pressure Fire-resistant Insulating Hose Assembly" technology being particularly outstanding. This technology, by embedding fire-resistant fibers and insulating materials in the rubber layer, enables the fire hose to maintain structural integrity for over 30 minutes at a high temperature of 1000℃, effectively preventing the spread of fires in well control accidents. This technology has been designated as a high-tech product for the update and replacement of well control devices by the former China National Petroleum Corporation and the China Petroleum Materials and Equipment Corporation, and has been widely applied in many oilfield projects of PetroChina and Sinopec.
Chapter 3: Application Experience: Full-scenario Coverage from Land to Sea
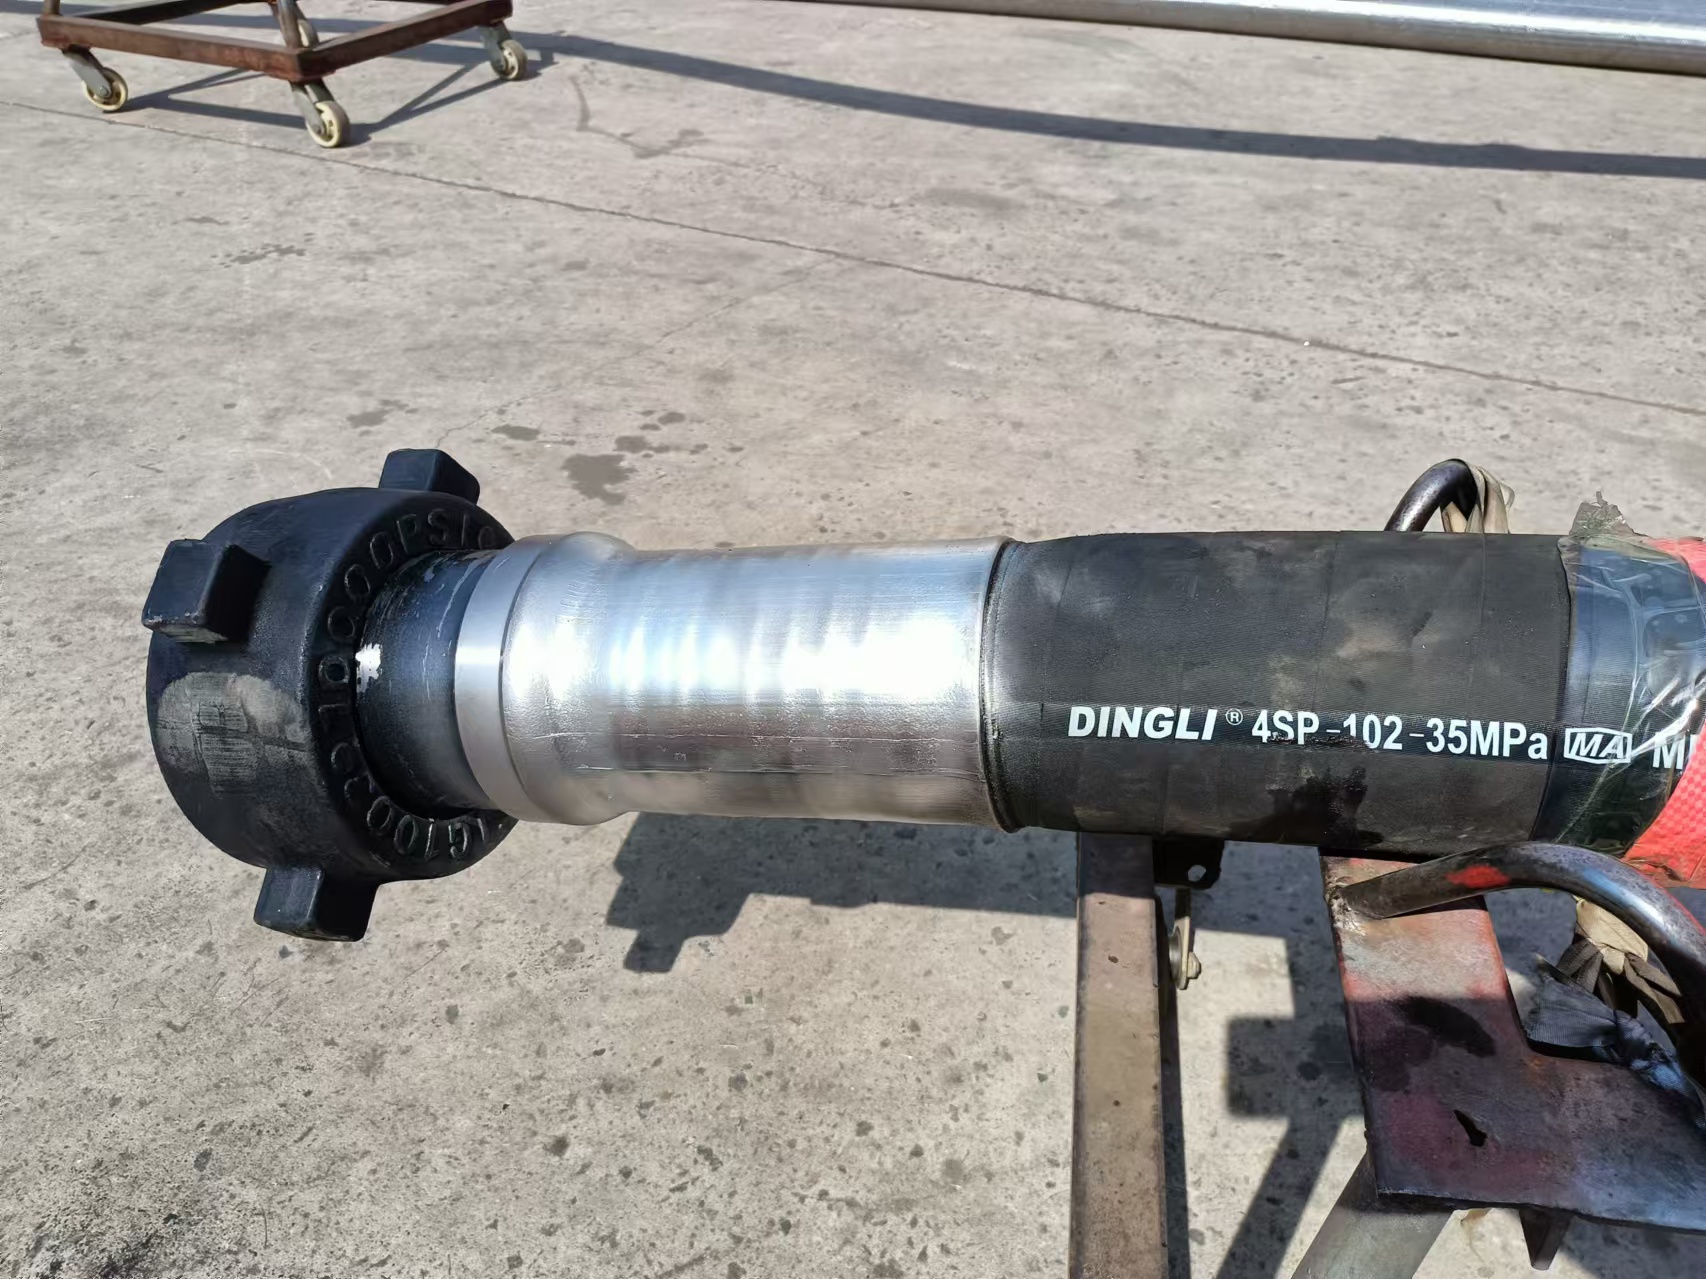
Hebei Dingli Pipeline Industry's firehose products have been widely promoted in domestic onshore and offshore oil fields and exported to more than a dozen countries and regions including Russia, Thailand, Australia, Canada, etc. Taking a certain offshore oilfield project of PetroChina as an example, the oilfield is located in the Bohai Bay with a water depth of up to 30 meters and a wellhead pressure as high as 70MPa, which puts extremely high requirements on the firehose's pressure resistance, corrosion resistance, and fatigue resistance. According to the project requirements, Dingli Pipeline Industry customized an enhanced firehose, which increased the number of steel wire braiding layers and optimized the rubber formula, raising the product's pressure resistance to 100MPa, corrosion resistance (salt spray test) to 1000 hours without rust, and fatigue resistance (bending test) to over 100,000 times without cracks. This product has been used continuously in the oilfield for 3 years without any failure, significantly reducing maintenance costs and downtime.
In land oilfield applications, Dingli Pipeline Industry's hoses also excel. For instance, in a drilling operation at an oilfield in Xinjiang, the wellhead temperature often reaches 80℃, and sandstorms are frequent, posing challenges to the hoses' temperature resistance and wear resistance. By using special rubber formulations and surface coating technology, the hoses maintain flexibility at 80℃ high temperatures and achieve a surface hardness of 65 Shore D, effectively resisting sand particle abrasion. The lifespan of this product at the oilfield is extended by 50% compared to traditional products, earning high recognition from users.
Four, Technical Cooperation: Joint Promotion of Innovation and Upgrade by Industry, University, and Research Collaboration
To continuously enhance technological strength, Hebei Dingli Pipe Industry has established long-term cooperative relationships with several universities and scientific research institutions. For instance, the company has jointly launched a research and development project on "new high-temperature-resistant rubber materials" with a material college of a university. By introducing nanofillers and crosslinking technology, the temperature resistance of rubber has been improved from 150℃ to 200℃, while maintaining excellent mechanical properties. This achievement has been applied to the company's high-end water hose products, making them more adaptable under extreme working conditions such as ultra-deep wells and high-temperature wells.
In addition, the company has collaborated with a scientific research institution to develop the "Intelligent Hose Monitor System," which embeds sensors within the hose to monitor parameters such as pressure, temperature, and deformation in real-time and transmits the data to the control center. Upon detecting any anomalies, the system immediately triggers an alarm, helping users identify potential faults in advance and prevent accidents. This technology has been pilot applied in an oilfield of Sinopec with significant effects and is expected to be widely promoted across the industry in the future.
V. Future Outlook: Leading with Technology, Serving Global Oil Fields
Hebei Dingli Pipeline Industry Co., Ltd. will continue to adhere to the development strategy of "technology as the guide," increase investment in research and development in material science, intelligent manufacturing, the Internet of Things, and continuously enhance the performance and intelligence level of hose products. At the same time, the company will take "product and character go hand in hand" as its corporate creed, and "sincere, honest, and earnest" as the service tenet, providing overseas oilfield users with higher-quality products and more considerate services, making greater contributions to China's land and marine oil exploration and development as well as the global oil industry.