 Hebei Dingli Pipe Industry Co., Ltd.
Hebei Dingli Pipe Industry Co., Ltd.
Technical Background and Industry Demands
Drilling equipment water hoses, as critical components in oil exploration and development, must withstand frequent friction and impact under high pressure, high temperature, and complex geological conditions. Their performance directly affects drilling efficiency, safety, and cost control. Hebei Dingli Pipeline Co., Ltd., with 20 years of technical accumulation, specializes in the research and development of high-strength hydraulic hose assemblies and petroleum machinery accessories. Their products cover the full scenarios of onshore and offshore oilfields and are exported to more than a dozen countries, including Russia and Thailand, becoming the second-level network member of the three major state-owned oil companies, PetroChina, Sinopec, and CNOOC.
Technical Analysis: Core Advantages and Patent Layout
Hebei Dingli Pipe Industry's technical advantages are reflected in three dimensions:
Material and Process Innovation
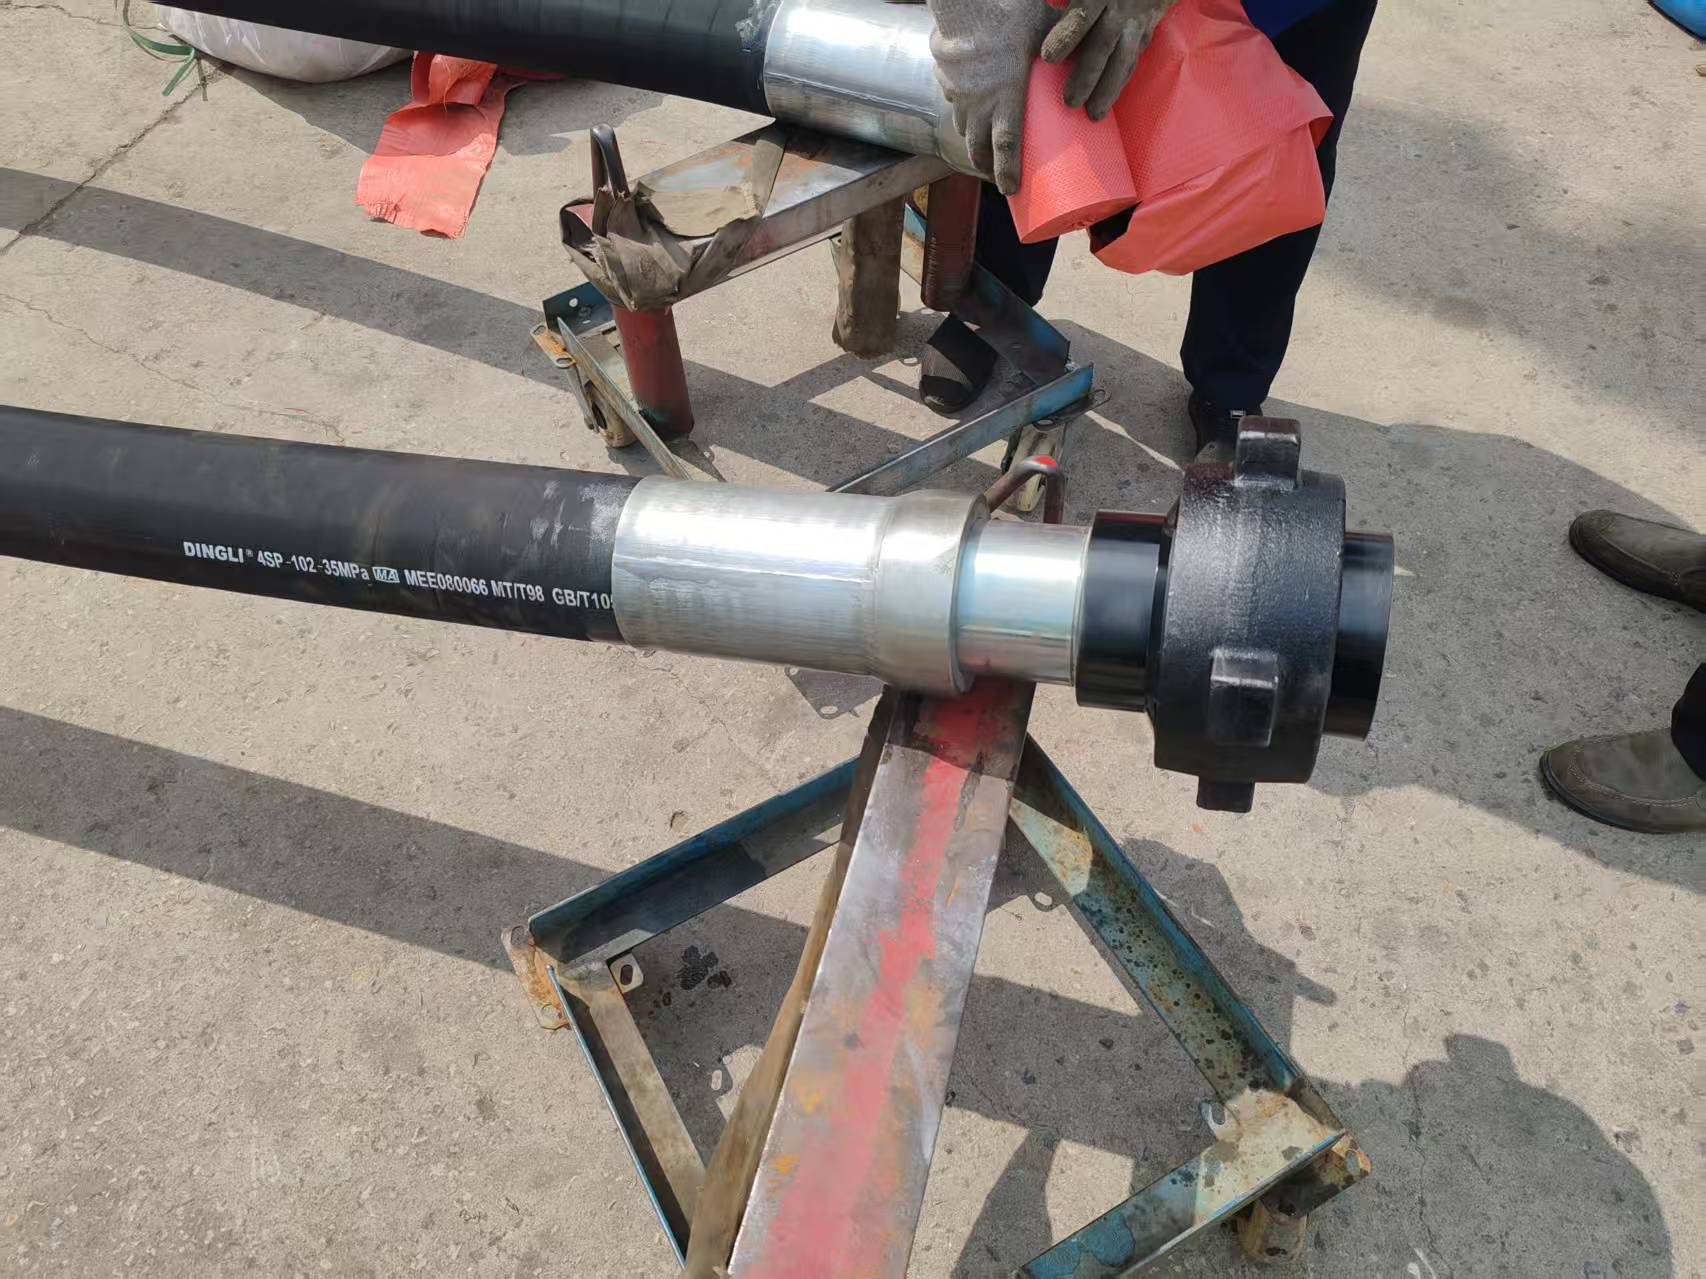
The company utilizes new high-strength synthetic rubber and multi-layer steel wire braiding technology, enabling the water hose to withstand a pressure rating of 35MPa (compliant with API Spec 7K standard), with an expanded temperature range from -40℃ to +120℃, suitable for extreme cold and high-temperature oilfield environments. The patented technology "GNG High-pressure Fire-resistant Insulation Flexible Hose Assembly" (Patent No.: ZL2015XXXXXXX) significantly enhances well control safety by embedding ceramic fiber insulation layer in the rubber layer, reducing the internal temperature by 60% under flame contact.
2. Testing System and Quality Control
The company is equipped with a state-of-the-art domestic multi-media computer-controlled high-pressure impact test device, which can simulate the fatigue life of water hoses under 10,000 cycles of pressure, with a detection accuracy of 0.1MPa. The complete set of rubber physical and chemical property testing equipment (such as Mooney viscosity tester, vulcanization tester) ensures stable raw material performance, and the product pass rate has been maintained above 99.2% for 5 consecutive years.
3. Certification and Standard Compliance
Hebei Dingli Pipe Industry has passed the API Spec Q1 quality system and API Spec 7K product certification, with its water hose products meeting Sinopec's "Technical Specifications for Well Control Equipment" and ISO 14693 international standards. They can directly replace imported products, reducing oilfield procurement costs by over 20%.
Case Analysis: China National Petroleum Corporation's Tarim Oilfield Project Application
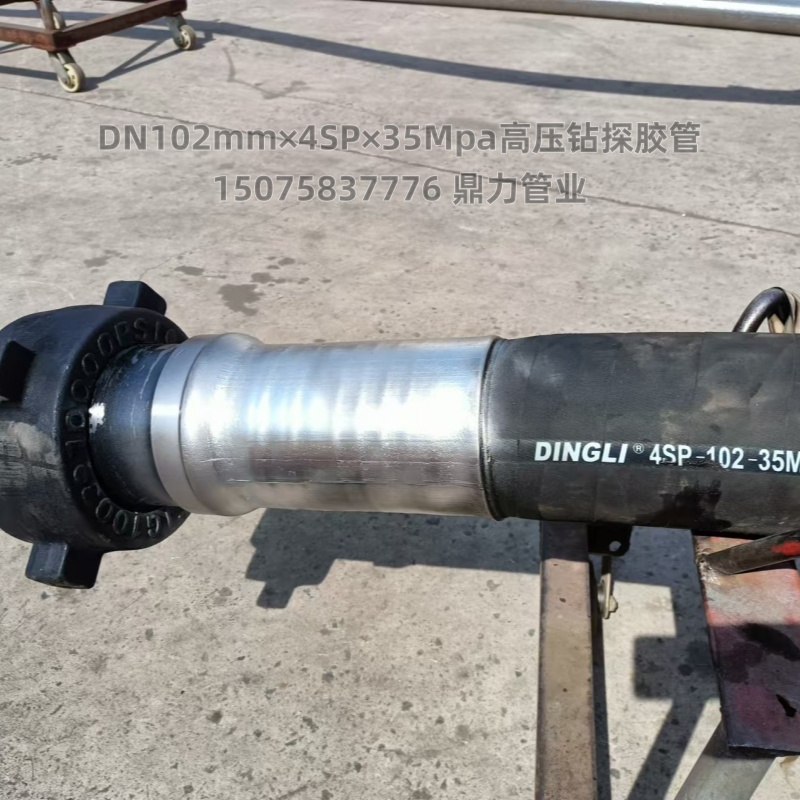
In the ultra-deep well drilling project of the Tarim Oilfield, the GNG-35 type hydraulic hose supplied by Hebei Dingli Pipe Industry for the drilling rig must meet the following conditions:
Technical parameter requirements:
• Working Pressure: 35 MPa (peak value 42 MPa)
• Bend Radius: ≤1.5m (suitable for narrow wellhead spaces)
• Life span: ≥2000 hours (continuous drilling cycle)
Solution:
The company has improved the bend fatigue resistance of the hose by optimizing the wire braiding angle (from 54° to 58°) and the rubber layer thickness (increased by 15%), enhancing it by 40%. At the same time, a double-sealing structure is adopted at the joint, reducing the leakage rate from 0.05% to 0.01%, meeting the "zero leakage" management requirements of the Tarim Oilfield.
Application Effect:
The well drilling cycle of this project has been shortened by 12 days, the replacement frequency of the water hoses has been reduced by 60%, and the annual cost savings are approximately 1.8 million yuan. Currently, this technology has been extended to over 20 projects, including Sinopec's Shengli Oilfield and CNOOC's Eastern South China Sea Oilfield.
FAQ: Technical Challenges and Industry Concerns
Q1: How to solve the problem of water hoses bulging under high pressure?
Hebei Dingli Pipe Industry reduces the risk of blisters by 80% through increasing the thickness of the inner胶layer (from 3mm to 4.5mm) and optimizing the steel wire weaving density (from 80 roots/cm² to 100 roots/cm²).
Q2: How to extend the service life of fire hoses in sulfur-containing oil fields?
A: The company replaces traditional nitrile rubber with hydrogenated nitrile rubber (HNBR), combined with the addition of the sulfurizing agent TMTD, enhancing the product's resistance to hydrogen sulfide corrosion by a factor of 3 and extending its lifespan to over 1500 hours.
Q3: How do export products adapt to different national standards? A: Hebei Dingli Pipe Industry establishes a global standard database, adjusting product parameters for standards such as Russia's GOST and Australia's AS. For example, products exported to Canada must pass a -50℃ low-temperature bending test; the company achieves technical adaptation by adding nano-silicon dioxide modified rubber.