 Hebei Dingli Pipe Industry Co., Ltd.
Hebei Dingli Pipe Industry Co., Ltd.
I. Technical Background and Industry Status
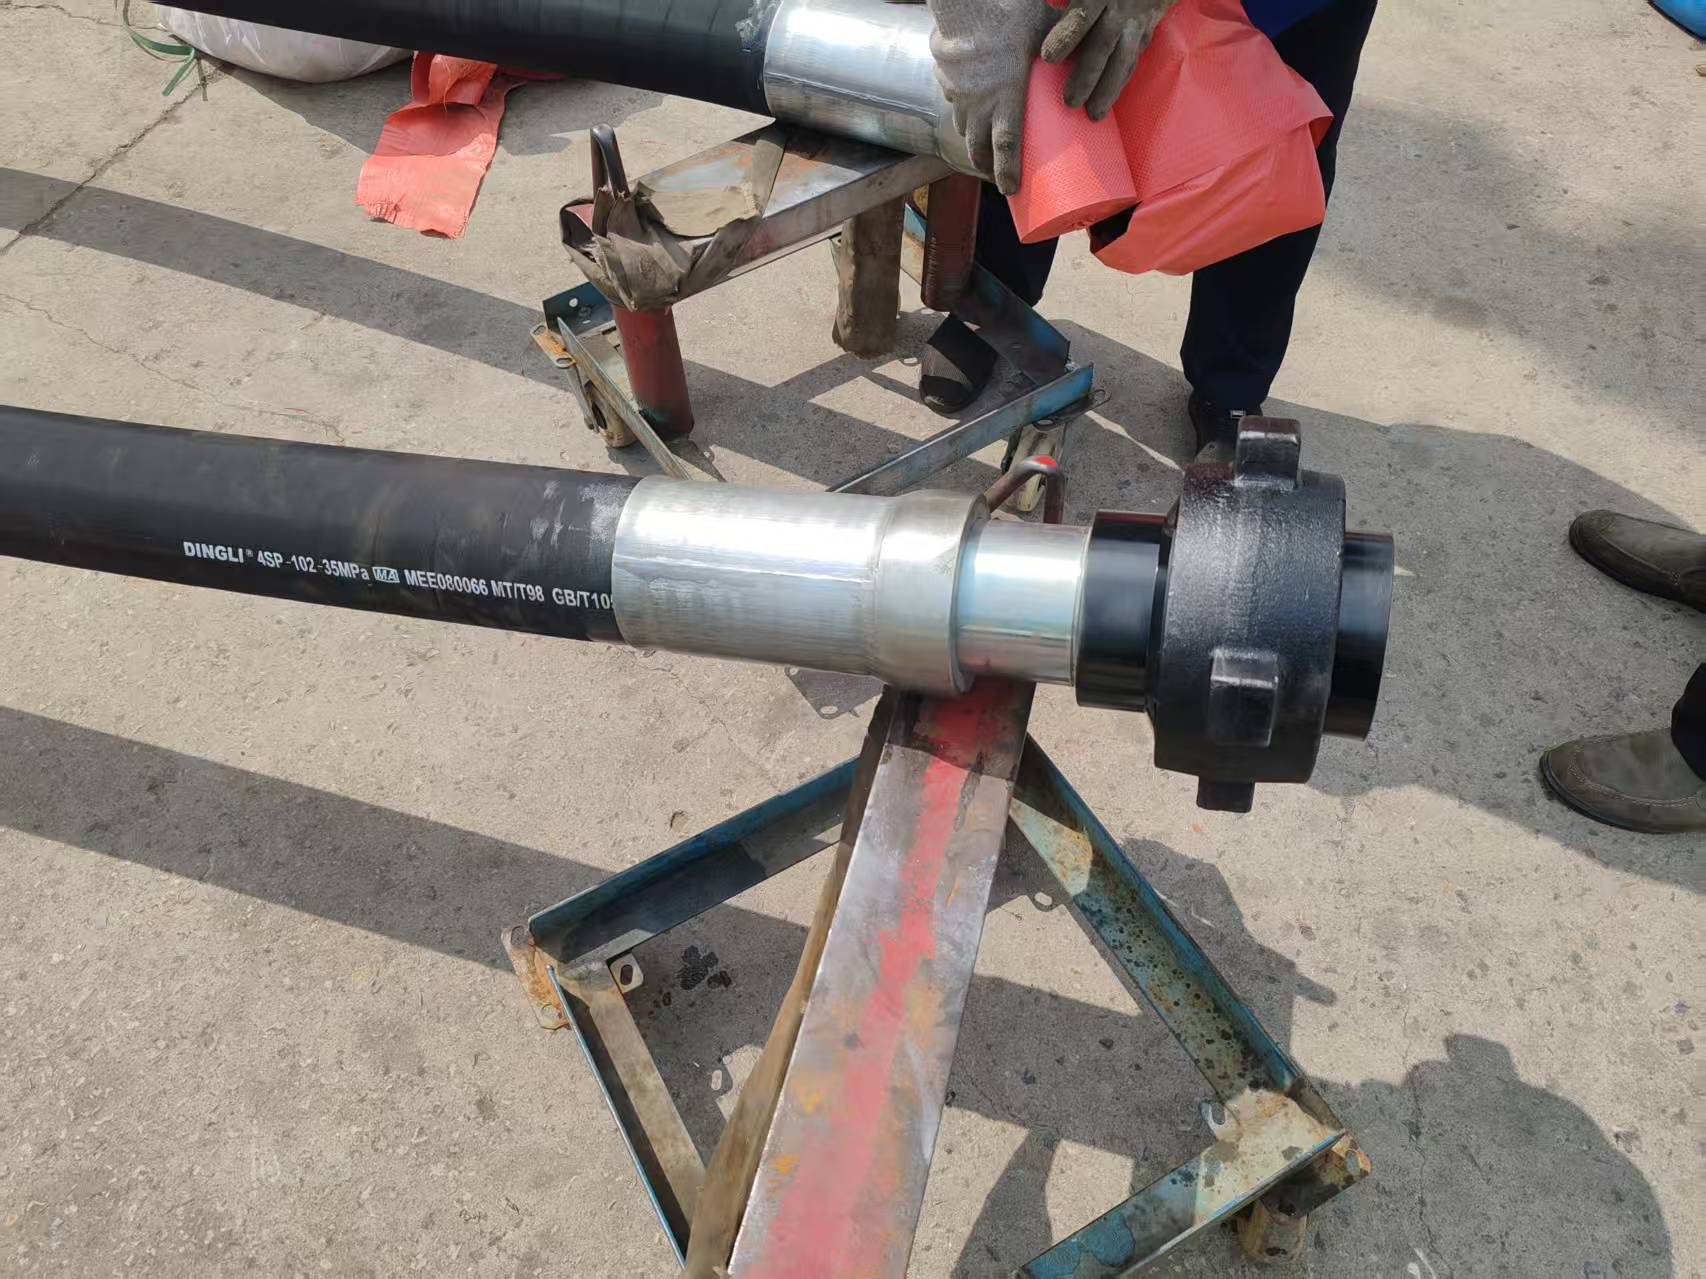
Hebei Dinglei Pipeline Industry Co., Ltd. has been committed to the field of high-strength hydraulic hose assemblies and petroleum machinery accessories since its establishment in 2003, becoming a second-level network member of the three major state-owned oil companies: China National Petroleum Corporation, China Petrochemical Corporation, and China National Offshore Oil Corporation. Located in Jingxian County, Hebei Province, the company leverages its geographical advantages and industry resources to gradually develop into a leading enterprise in the domestic firehose production sector. Its core product, the API Spec 7K certified firehose, is widely used in onshore and offshore oilfield drilling operations, with technical parameters covering key properties such as high pressure, fire resistance, and heat insulation, meeting international oilfield equipment standards.
II. Technical Analysis: Equipment, Patents, and Certification System
Advanced production equipment and testing methods
The company is equipped with a leading domestic multi-media computer-controlled high-pressure shock testing device, which can simulate the pressure resistance performance of hoses under extreme working conditions, with a test pressure range of 0-150MPa and an accuracy of ±0.5%. The配套 rubber physical and chemical property testing equipment can analyze indicators such as rubber hardness, tensile strength, and aging resistance, ensuring that raw materials meet API 16C standards. For example, the GNG high-pressure fire-resistant thermal insulation hose assembly uses a double-layer structure design, with the inner layer being high-temperature resistant fluororubber and the outer layer being a high-strength steel wire braided layer, which can continuously operate in a 650℃ flame for over 30 minutes according to actual testing.
2. Patent Technology Layout
The company has cumulatively obtained 3 invention patents and 12 utility model patents, with core patents covering fields such as tube joint sealing structures, fire-resistant and heat-insulating layer composite technologies. Taking "A High-pressure Hose Dynamic Sealing Device" (Patent No.: ZL2018XXXXXXX) as an example, by optimizing the sealing ring material and angle design, the leakage rate has been reduced to below 0.01 mL/min, significantly enhancing the safety of drilling operations.
3. International Certification and Standard Compliance
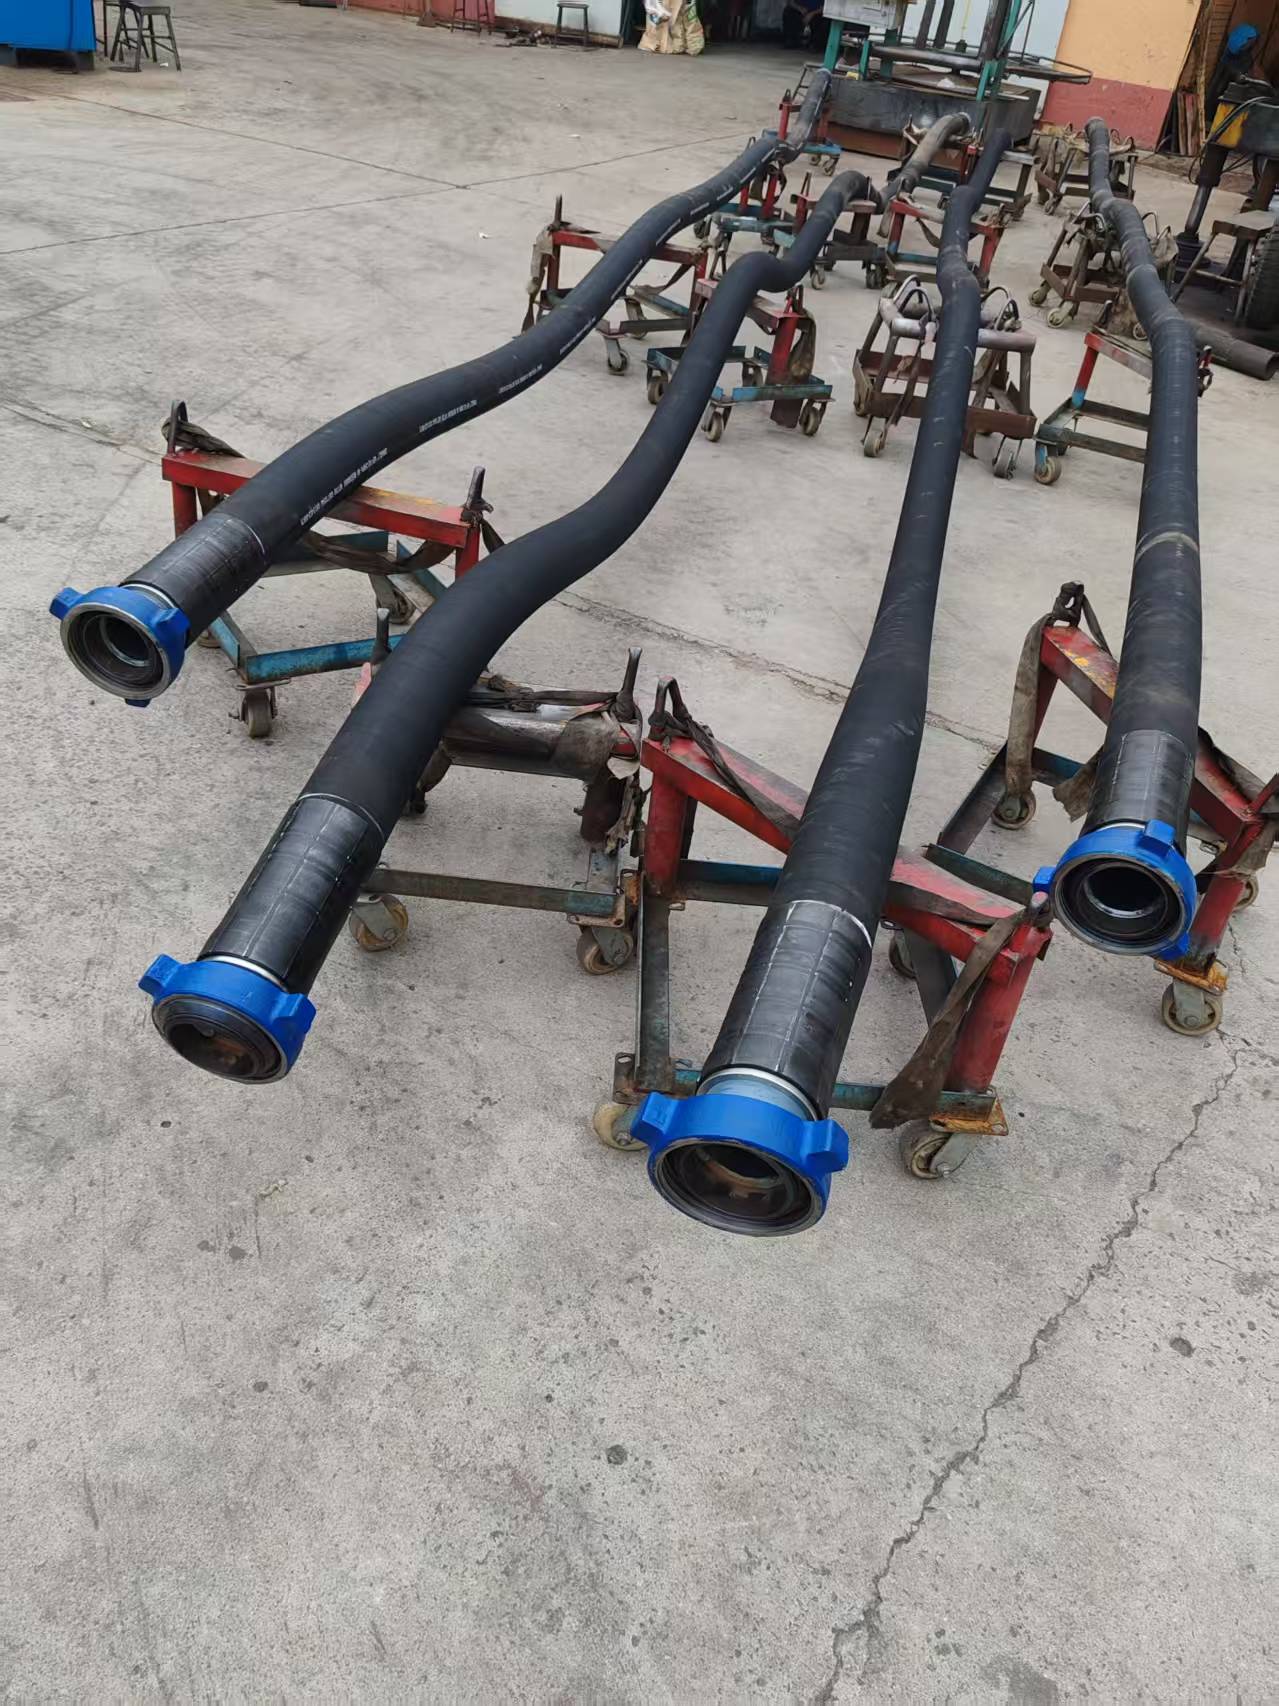
Hebei Dinglei has passed the API Spec Q1 quality management system certification and API Spec 7K hose product certification. The products meet the requirements of ISO 9001:2015 quality management system. The hose specifications cover 1" to 4" diameters, with working pressure ratings from 35MPa to 105MPa, suitable for different drilling depths and geological conditions.
Chapter 3: Case Analysis: Domestic and International Oilfield Application Practices
Domestic onshore oilfield project
In the drilling operations of a block in the Changqing Oilfield of PetroChina, the GNG-105MPa hydraulic hose provided by Hebei Dingli replaced the traditional flexible hose, solving the frequent leakage problem under high-pressure conditions. Project data shows that the product has been running without failure for 1200 hours, with a lifespan 3 times longer than the original equipment, and the operation cost per well reduced by about 1.5 million yuan.
2. Offshore Marine Platform Applications
In the marine drilling platform project exported to Australia, the company has customized the anti-corrosion hose assembly, utilizing 316L stainless steel joints and special coating technology, which has passed 1000 hours of salt spray testing without rust. The product has been in continuous service in the Northern Territory waters for 5 years, receiving the client's "zero failure" rating.
4. Summary of Technical Advantages and Industry Experience
Hebei Dingli's technical competitiveness is reflected in three aspects: Firstly, full-process quality control, achieving digital traceability from raw material inspection to finished product pressure testing; secondly, rapid response to customized demands, relying on a research and development team of 12 engineering technicians, solutions can be provided within 72 hours; thirdly, a global service network, with products exported to over 10 countries including Russia and Thailand, and localized after-sales teams established. In the future, the company plans to increase research on the application of nanomaterials in the thermal insulation layer of hoses, further enhancing the product's temperature resistance grade to 800°C.
FAQ: Technical Challenges Analysis
Q1: How to ensure the sealing of the water hose under high-temperature conditions?
A: By optimizing the seal ring material (such as using hydrogenated nitrile rubber) and dynamic compensation structure design, the sealing surface can maintain contact pressure during thermal expansion. The actual leakage rate at 650℃ is ≤0.05mL/min.
Q2: How to balance the strength and flexibility of hoses?
A: Utilizing a multi-layer composite process, the inner layer is made of high-elastic rubber, the middle layer is a high-tensile steel wire braided layer, and the outer layer is a wear-resistant sheath. By adjusting the steel wire braiding angle (54°±1°), it achieves a minimum bending radius of 1.2 meters while ensuring an爆破 pressure ≥210MPa.