In the demanding world of oilfield operations, efficient mud transport systems are critical for maintaining drilling productivity and safety. Hebei Dingli Pipe Industry Co., Ltd., established in 2003 in Jing County, Hebei Province – the hometown of the renowned Confucian scholar Dong Zhongshu – has emerged as a global leader in manufacturing specialized equipment for this essential application. As a key supplier to China National Petroleum Corporation (CNPC), China Petroleum & Chemical Corporation (Sinopec), and China National Offshore Oil Corporation (CNOOC), our company has developed a comprehensive range of mud transport solutions that meet the stringent requirements of modern drilling operations worldwide.
Comprehensive Mud Transport System Solutions
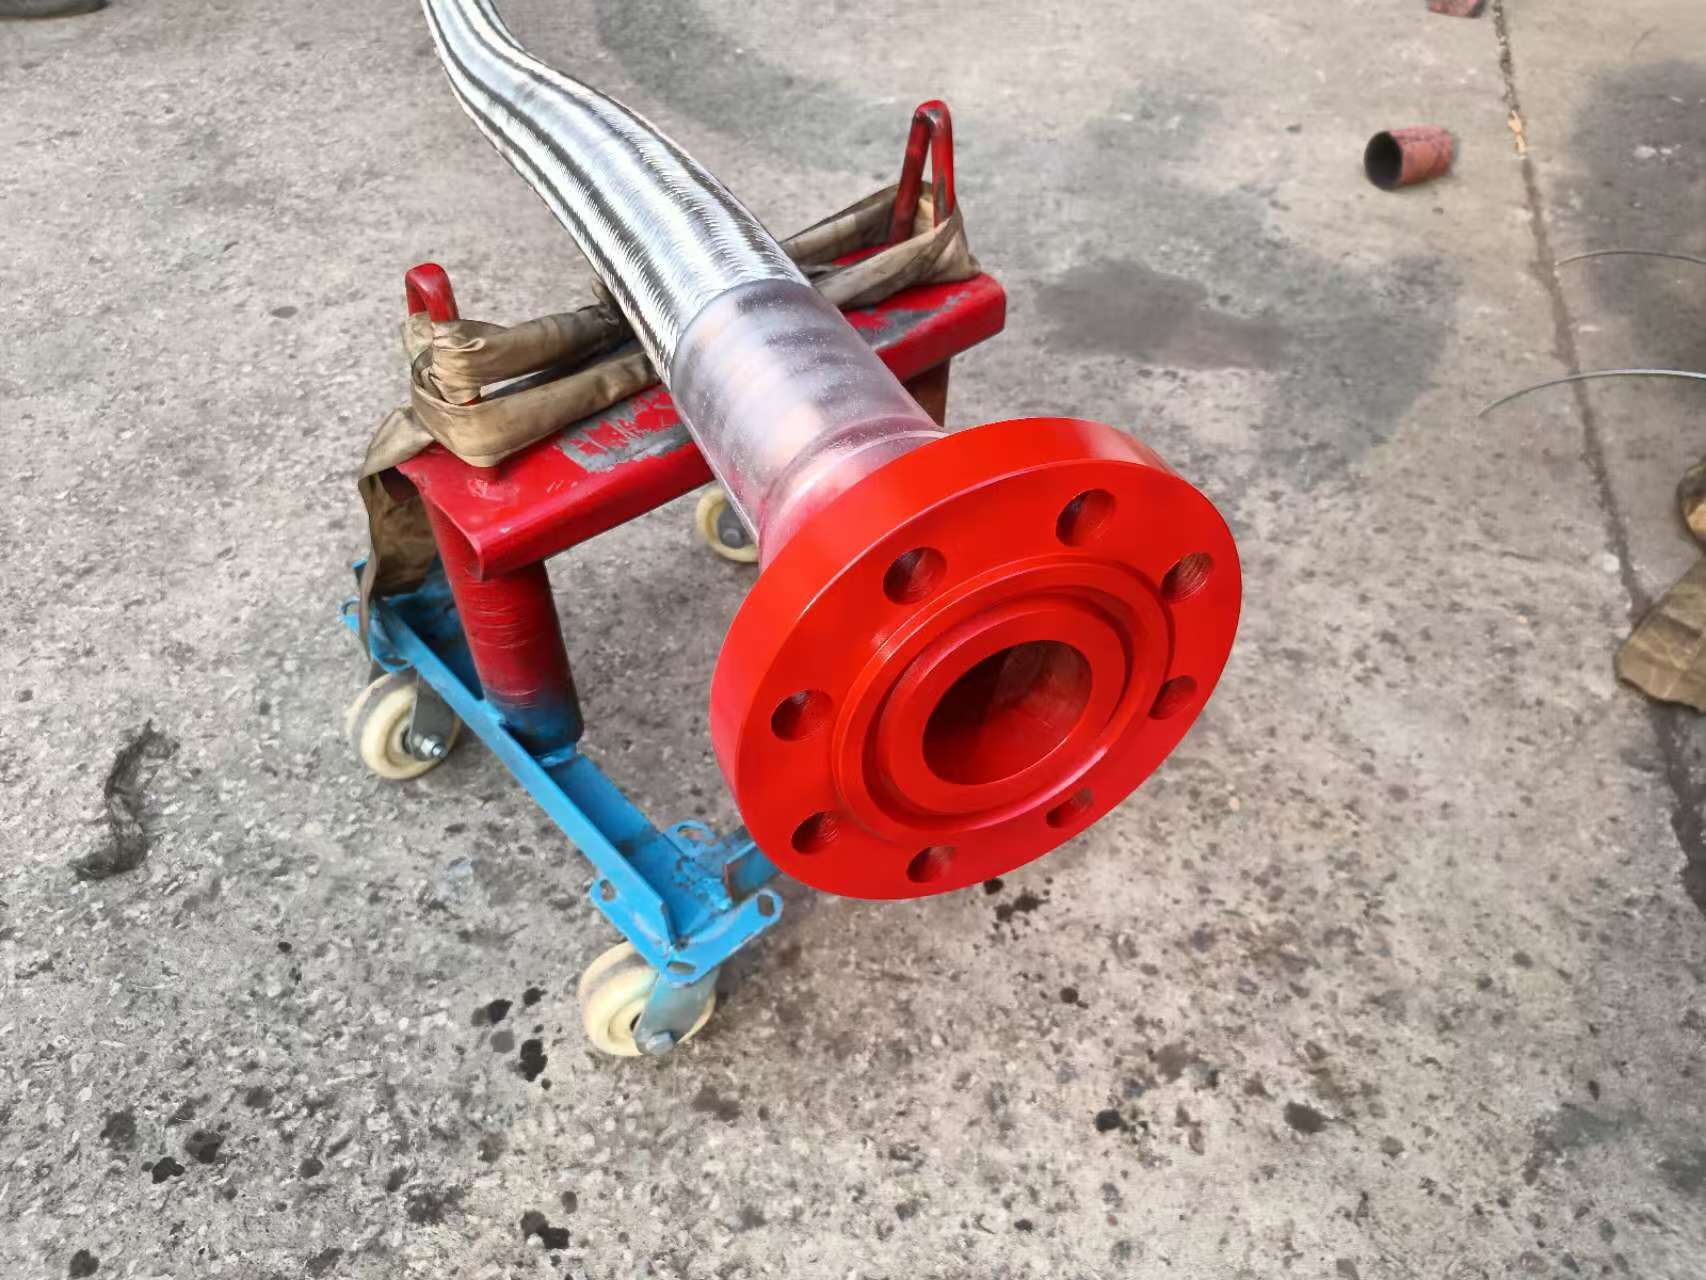
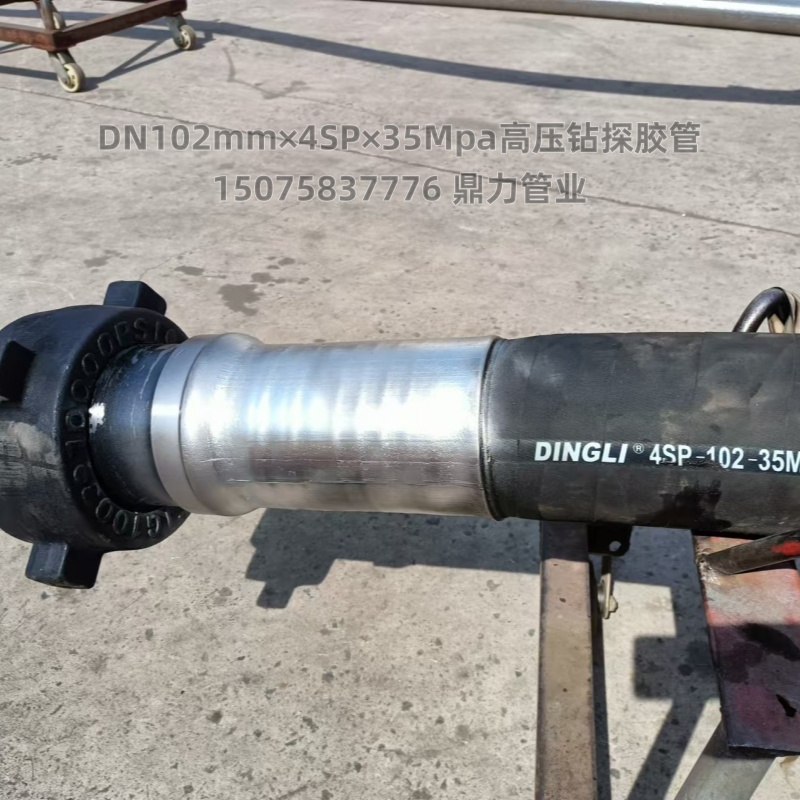
Our product portfolio addresses all aspects of mud transport in oilfield operations. The core of our offerings includes high-strength hydraulic hose assemblies specifically designed for the rigorous demands of mud circulation systems. These hoses feature reinforced construction using advanced synthetic materials that withstand extreme pressures, abrasive particles, and corrosive chemicals commonly found in drilling mud. Our engineering team has developed specialized formulations that extend service life while maintaining flexibility for easy installation and handling in challenging field conditions.
Complementing our hose assemblies are precision-engineered petroleum machinery parts that form the backbone of mud transport systems. These components include high-pressure connectors, swivel joints, and manifold systems that ensure reliable fluid transfer with minimal pressure drop. Each part undergoes rigorous testing to verify performance under simulated operating conditions, including pressure cycling tests up to 10,000 psi and temperature extremes from -40°C to +120°C. This attention to detail guarantees that our systems maintain consistent performance throughout their service life, reducing downtime and maintenance costs for our clients.
Technological Advantages in Mud Transport Systems
What sets Hebei Dingli apart in the competitive mud transport equipment market is our unwavering commitment to technological innovation. Our state-of-the-art manufacturing facility houses the most advanced multimedia computer-controlled high-pressure impact testing equipment in China, allowing us to simulate decades of field service in a matter of hours. This capability enables rapid product development cycles and ensures that our designs meet or exceed international standards before they reach customers.
Our R&D team works closely with leading universities and research institutions to incorporate the latest material science breakthroughs into our products. Recent innovations include the development of self-lubricating composite materials for hose liners that reduce friction and wear, and intelligent monitoring systems that provide real-time performance data to drilling crews. These technological advancements have resulted in mud transport solutions that offer 30% longer service life compared to conventional designs while improving overall system efficiency by up to 15%.
API Certification and Global Recognition
The quality of our mud transport systems is formally recognized through our API Spec Q1 quality management system certification and API Spec 7K product certification for drilling hoses. These international accreditations demonstrate our compliance with the highest industry standards for product safety, reliability, and performance. Our facilities undergo regular audits by API inspectors to ensure ongoing adherence to these rigorous requirements, giving our customers confidence in the consistency and quality of our products.
This commitment to excellence has earned us recognition as a Provincial Excellent Technology Enterprise in Hebei and consecutive awards as a Policy Implementation Advanced Unit and Contract-Honoring Credit-Keeping Enterprise. More importantly, it has established us as a preferred supplier to major oil companies worldwide, with our products currently in service in oilfields across Russia, Thailand, Australia, Canada, and other key markets.
| Product Category | Key Features | Application |
|---|---|---|
| High-Pressure Mud Hoses | Up to 10,000 psi working pressure, abrasion-resistant lining, temperature-resistant construction | Mud circulation systems, drilling rigs, well control equipment |
| Swivel Joints | 360° rotation, metal-to-metal seals, high-pressure rated | Mud manifold systems, cementing units, fracturing equipment |
| Quick Connectors | Double-bolt locking, pressure-balanced design, easy operation | Mud pump discharge, high-pressure mud lines, BOP systems |
Global Supply Chain and Customization Capabilities
Understanding the diverse requirements of international oilfield operations, we have established a flexible manufacturing system capable of producing both standard products and customized solutions. Our engineering team works closely with clients to develop mud transport systems tailored to specific operating conditions, including extreme temperatures, corrosive environments, or unique space constraints on offshore platforms.
This customization capability extends to our global supply chain, which ensures timely delivery of products to any location worldwide. We maintain strategic stocking points in key regions and work with trusted logistics partners to provide just-in-time delivery services. Our international sales team, fluent in multiple languages, provides comprehensive technical support throughout the project lifecycle, from initial design consultation to after-sales service.
FAQ
What certifications do your mud transport hoses have for international use?
Our mud transport hoses are certified to API Spec 7K standards and manufactured under our API Spec Q1 certified quality management system. These certifications ensure compliance with the highest international standards for drilling hose performance and safety, making our products suitable for use in any global oilfield operation.
How do your mud transport systems handle abrasive drilling fluids?
We incorporate specialized abrasion-resistant materials in our hose linings that provide 3-5 times longer service life compared to standard rubber compounds when transporting abrasive drilling muds. Additionally, our swivel joints and connectors feature hardened surfaces and advanced sealing technologies to prevent premature wear from abrasive particles.
What temperature ranges can your mud transport equipment withstand?
Our standard mud transport hoses are rated for continuous operation between -40°C and +120°C (-40°F to +248°F). For extreme temperature applications, we offer specialized formulations that maintain flexibility and strength at temperatures as low as -70°C (-94°F) or as high as +150°C (+302°F).
Can you provide complete mud transport systems or just individual components?
As a full-service manufacturer, we can supply both individual components and complete turnkey mud transport systems. Our capabilities include system design, component manufacturing, assembly, testing, and installation supervision. Many clients prefer our integrated approach as it ensures optimal component compatibility and system performance.
How do you ensure quality control in your manufacturing process?
Quality is embedded in every stage of our production process through our API-certified quality management system. This includes incoming material inspection, in-process quality checks, and final product testing using our advanced computer-controlled test equipment. Each mud transport hose undergoes pressure testing to 1.5 times its rated working pressure before shipment.
Summary
Hebei Dingli Pipe Industry Co., Ltd. stands as a premier global supplier of mud transport systems, combining advanced technology, rigorous quality standards, and customized solutions to meet the evolving needs of the oil and gas industry. With over two decades of experience serving the world’s leading energy companies, we have developed a comprehensive product range that addresses all aspects of mud circulation in drilling operations. Our API-certified equipment, manufactured in our state-of-the-art facility, delivers exceptional reliability and performance in the most demanding environments worldwide. By choosing Hebei Dingli as your mud transport system partner, you gain access to not just high-quality products, but also our technical expertise, global supply capabilities, and unwavering commitment to customer satisfaction.