In the competitive landscape of oilfield equipment manufacturing, Hebei Dingli Pipeline Co., Ltd. stands out as a premier producer of mud transport systems, high-strength hydraulic hose assemblies, and specialized petroleum machinery parts. Established in 2003 and located in Jing County, Hebei Province – the hometown of the renowned Confucian scholar Dong Zhongshu – our company has evolved into a critical manufacturing hub for China National Petroleum Corporation’s well control equipment配套 center (supporting center for well control equipment). As an original designated manufacturer of well control hoses for the former China National Petroleum Corporation, we maintain our status as a secondary network member across all three major Chinese oil groups: CNPC, Sinopec, and CNOOC.
Technological Excellence in Mud Transport System Manufacturing
Our production capabilities are anchored by advanced manufacturing equipment and rigorous quality control systems. The company operates China’s most sophisticated multimedia computer-controlled high-pressure impact testing device, along with comprehensive physical and chemical property testing equipment for rubber and hoses. This technological infrastructure enables us to maintain consistent product quality while achieving annual production value of approximately 200 million RMB (about US$28 million).
The engineering team, comprising 12 specialized technicians among our 50-strong workforce, focuses on developing innovative solutions for oilfield applications. Our R&D investments have yielded multiple invention patents and utility model patents, earning recognition as Hebei Province’s Outstanding Technology Enterprise. The company’s commitment to quality is further validated by our API Spec Q1 quality management system certification and API Spec 7K drilling hose product certification from the American Petroleum Institute.
Comprehensive Product Range for Global Oilfields
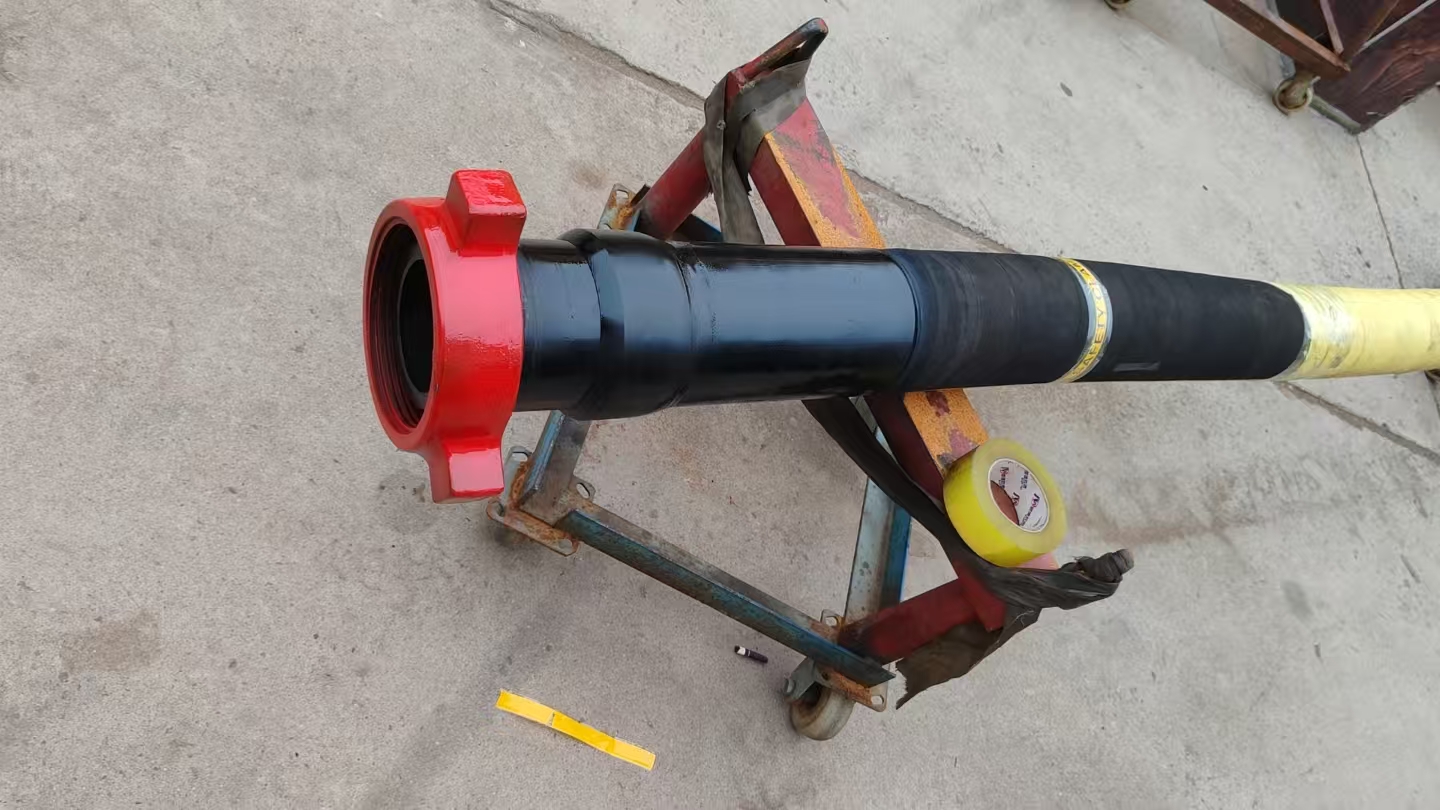
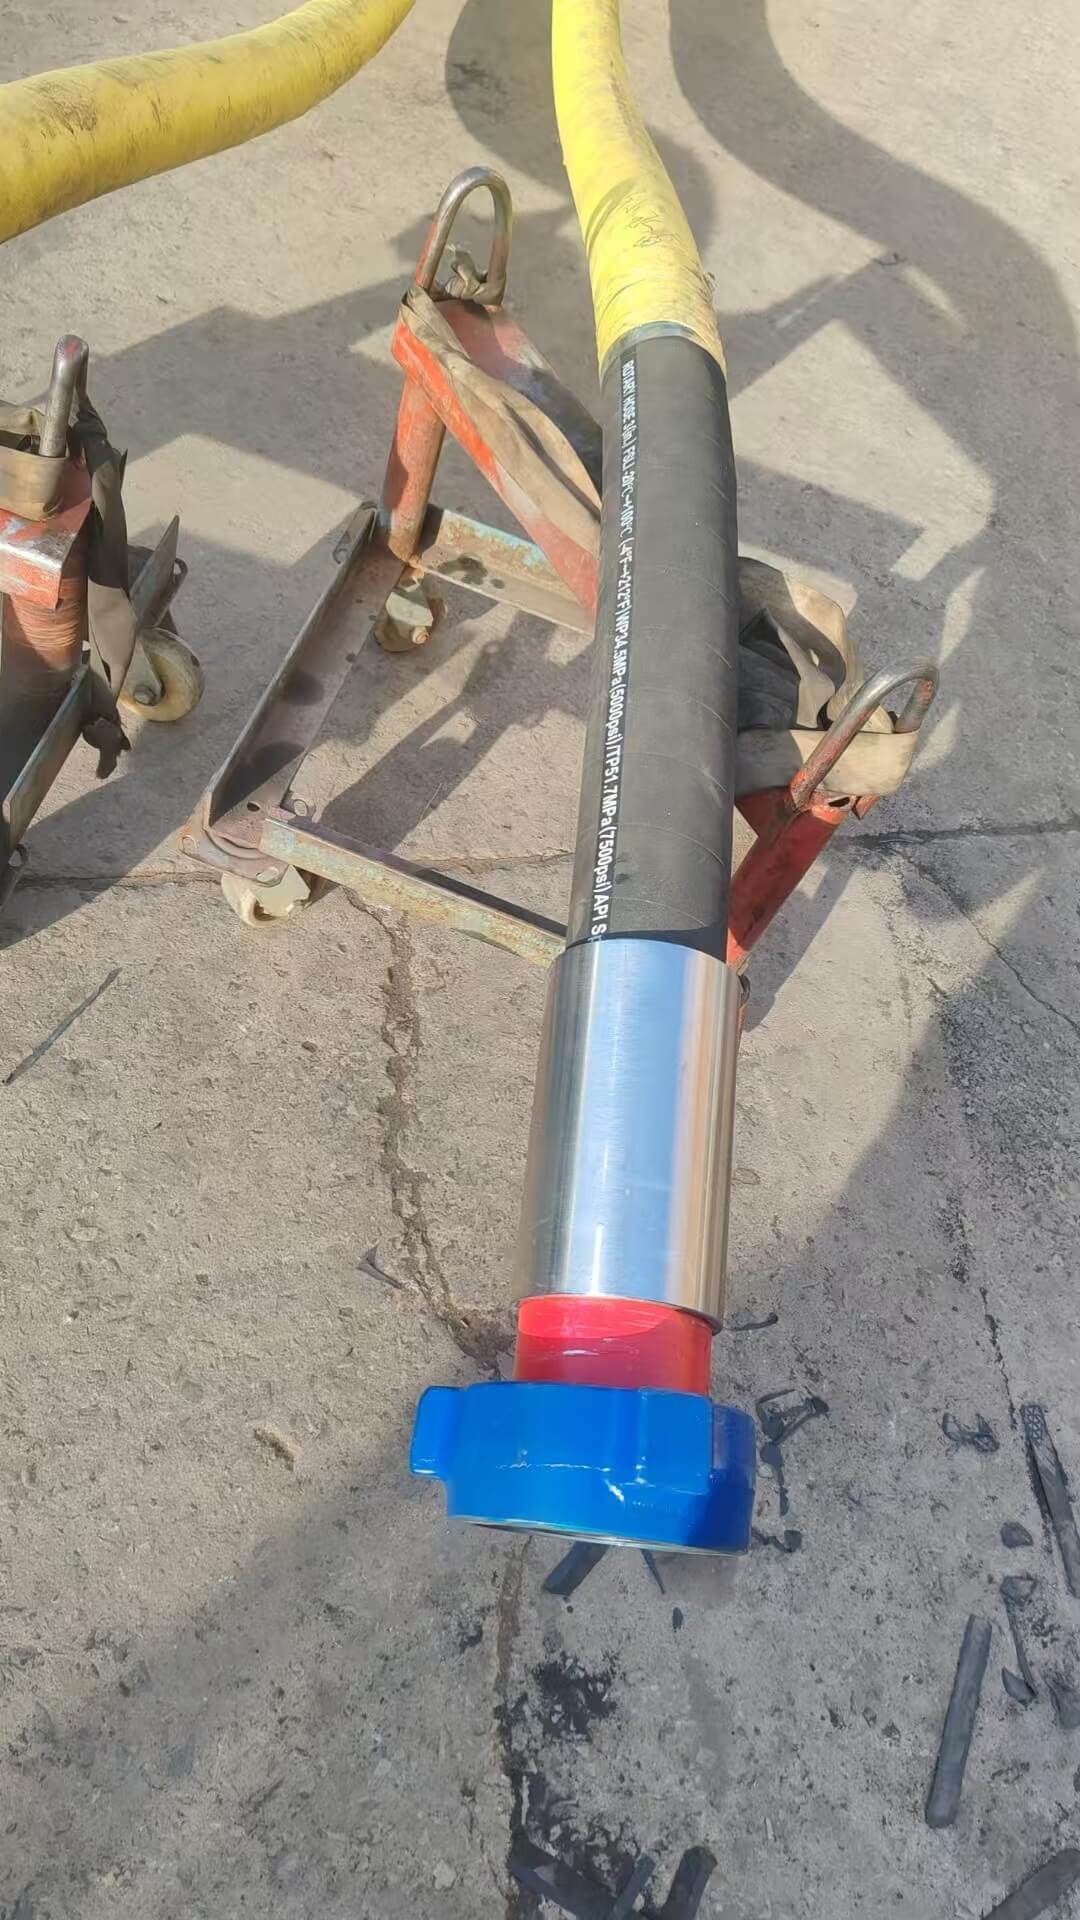
Over the past two decades, Hebei Dingli has developed twenty major product series that now serve oilfields worldwide. Our flagship GNG high-pressure fire-resistant heat-insulating hose assembly represents a technological breakthrough in well control equipment, having been designated as a high-tech upgrade product by both CNPC and China Petroleum Material & Equipment Corporation. This recognition established us as the exclusive export supplier of drilling and well control hose equipment for these industry giants.
Our product portfolio specifically addresses the demanding requirements of mud transport systems through:
- High-strength hydraulic hose assemblies rated for extreme pressures and temperatures
- Specialized couplings and connectors engineered for harsh oilfield environments
- Fire-resistant and heat-insulating hose technologies for enhanced operational safety
- Custom-designed solutions for specific drilling and well control applications
- Comprehensive testing protocols ensuring reliability in critical operations
Global Market Penetration and Industry Recognition
Hebei Dingli’s products have achieved complete market penetration across domestic and international oilfields, with exports reaching Russia, Thailand, Australia, Canada, and ten other countries. Our international success stems from three core competitive advantages:
| Competitive Advantage | Implementation Details |
|---|---|
| Technological Innovation | Collaboration with universities and research institutions to develop new materials and manufacturing processes |
| Quality Certification | API Spec Q1 and API Spec 7K certifications meeting international oil industry standards |
| Global Distribution | Established export channels serving major oil-producing regions worldwide |
Strategic Approach to Mud Transport System Development
Our R&D strategy focuses on addressing three critical challenges in mud transport systems: pressure resistance, thermal stability, and operational reliability. The GNG series hose assemblies exemplify this approach by integrating multiple patented technologies that enable:
- Continuous operation at temperatures exceeding 260°C (500°F)
- Pressure ratings up to 140 MPa (20,300 psi) for ultra-deep drilling applications
- Fire-resistant properties maintaining structural integrity during well blowouts
- Reduced maintenance requirements through advanced material formulations
- Compatibility with standard drilling equipment interfaces
These technical specifications have made our products essential components in modern drilling operations, particularly for high-pressure, high-temperature (HPHT) wells where conventional equipment fails. The GNG series’ ability to withstand extreme conditions while maintaining flexibility and ease of installation has set new industry benchmarks for well control hoses.
FAQ
What certifications do your mud transport systems hold?
Our products comply with API Spec Q1 quality management system standards and carry API Spec 7K certification for drilling hoses. These international certifications ensure our mud transport systems meet the stringent requirements of global oilfield operations.
How do you ensure product quality in mud transport systems?
Quality control begins with raw material inspection and continues through 17 manufacturing stages with 100% testing. Our multimedia computer-controlled high-pressure impact testing device simulates extreme operating conditions to validate product performance before shipment.
What makes your GNG series hoses different from competitors?
The GNG series incorporates patented fire-resistant and heat-insulating technologies that maintain structural integrity at temperatures exceeding 260°C. This unique combination of pressure resistance and thermal stability makes our hoses superior for demanding well control applications.
Can you customize mud transport systems for specific requirements?
Yes, our engineering team works closely with clients to develop tailored solutions. We can modify hose dimensions, pressure ratings, coupling types, and thermal properties to match specific drilling conditions and equipment configurations.
What is the lead time for manufacturing mud transport systems?
Standard products typically ship within 15-20 working days after order confirmation. Custom-designed systems require 25-35 working days for production, depending on complexity and component availability.
How do you handle international shipping and logistics?
We maintain established export channels with experienced freight forwarders specializing in oilfield equipment. Our logistics team coordinates all aspects of shipping, customs clearance, and documentation to ensure timely delivery to global destinations.
What warranty do you offer on your products?
All mud transport systems come with a 12-month warranty covering manufacturing defects. We provide comprehensive after-sales support including technical consultation, spare parts supply, and on-site maintenance assistance when required.
How does your company ensure continuous product improvement?
We allocate 8-10% of annual revenue to R&D, collaborating with universities and research institutions. This investment enables us to incorporate advanced materials and manufacturing processes, maintaining our technological leadership in mud transport systems.
Summary
Hebei Dingli Pipeline Co., Ltd. has established itself as a global leader in mud transport system manufacturing through technological innovation, rigorous quality control, and customer-focused service. Our API-certified products, including the revolutionary GNG series high-pressure hoses, set industry standards for performance and reliability in demanding oilfield environments. With exports to over 15 countries and recognition from major oil corporations, we continue to expand our international presence while maintaining the highest production standards. By combining advanced manufacturing capabilities with a commitment to continuous improvement, Hebei Dingli remains dedicated to supporting the global oil industry’s evolving needs with superior mud transport solutions.